OT-2026-000003258
Resistance projection welding system and method for welding a projection weld nut to a workpiece
- Published
- Permanent URL
- https://opentechnical.org/p/OT-2026-000003258
- Classification
- Manufacturing & Assembly Equipment › Joining and Welding
- Original source
- US-5632912-A, the United States Patent and Trademark Office, 27 May 1997
- Document SHA-256
- ff675cdb5e697cb9364f57ccbb963bd208bf3d2d646fa33e94d49aa9a34e7aef
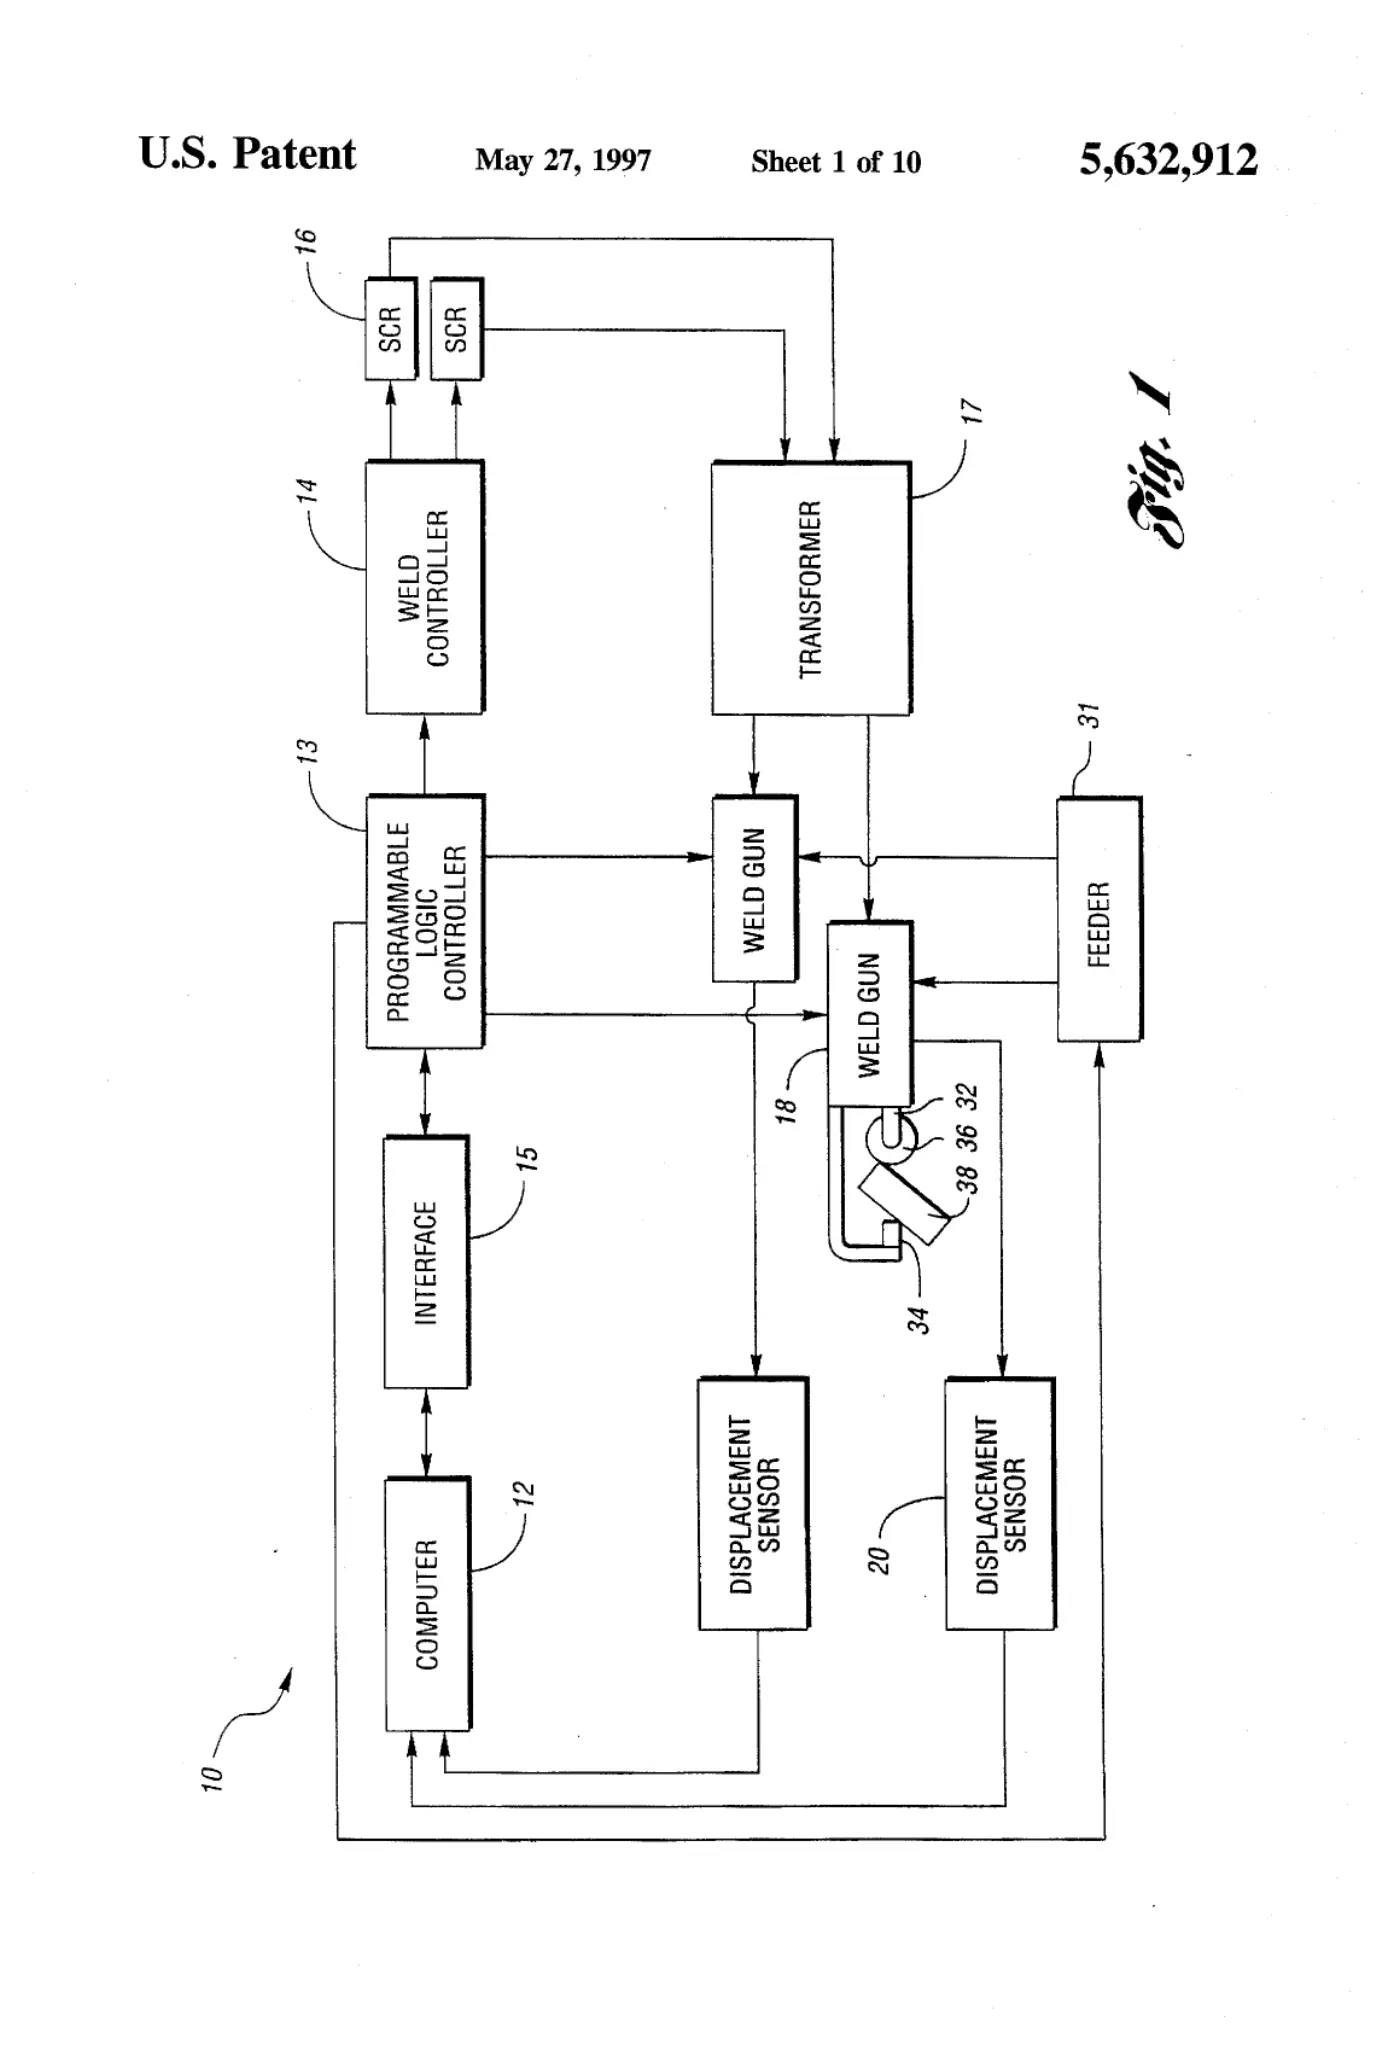
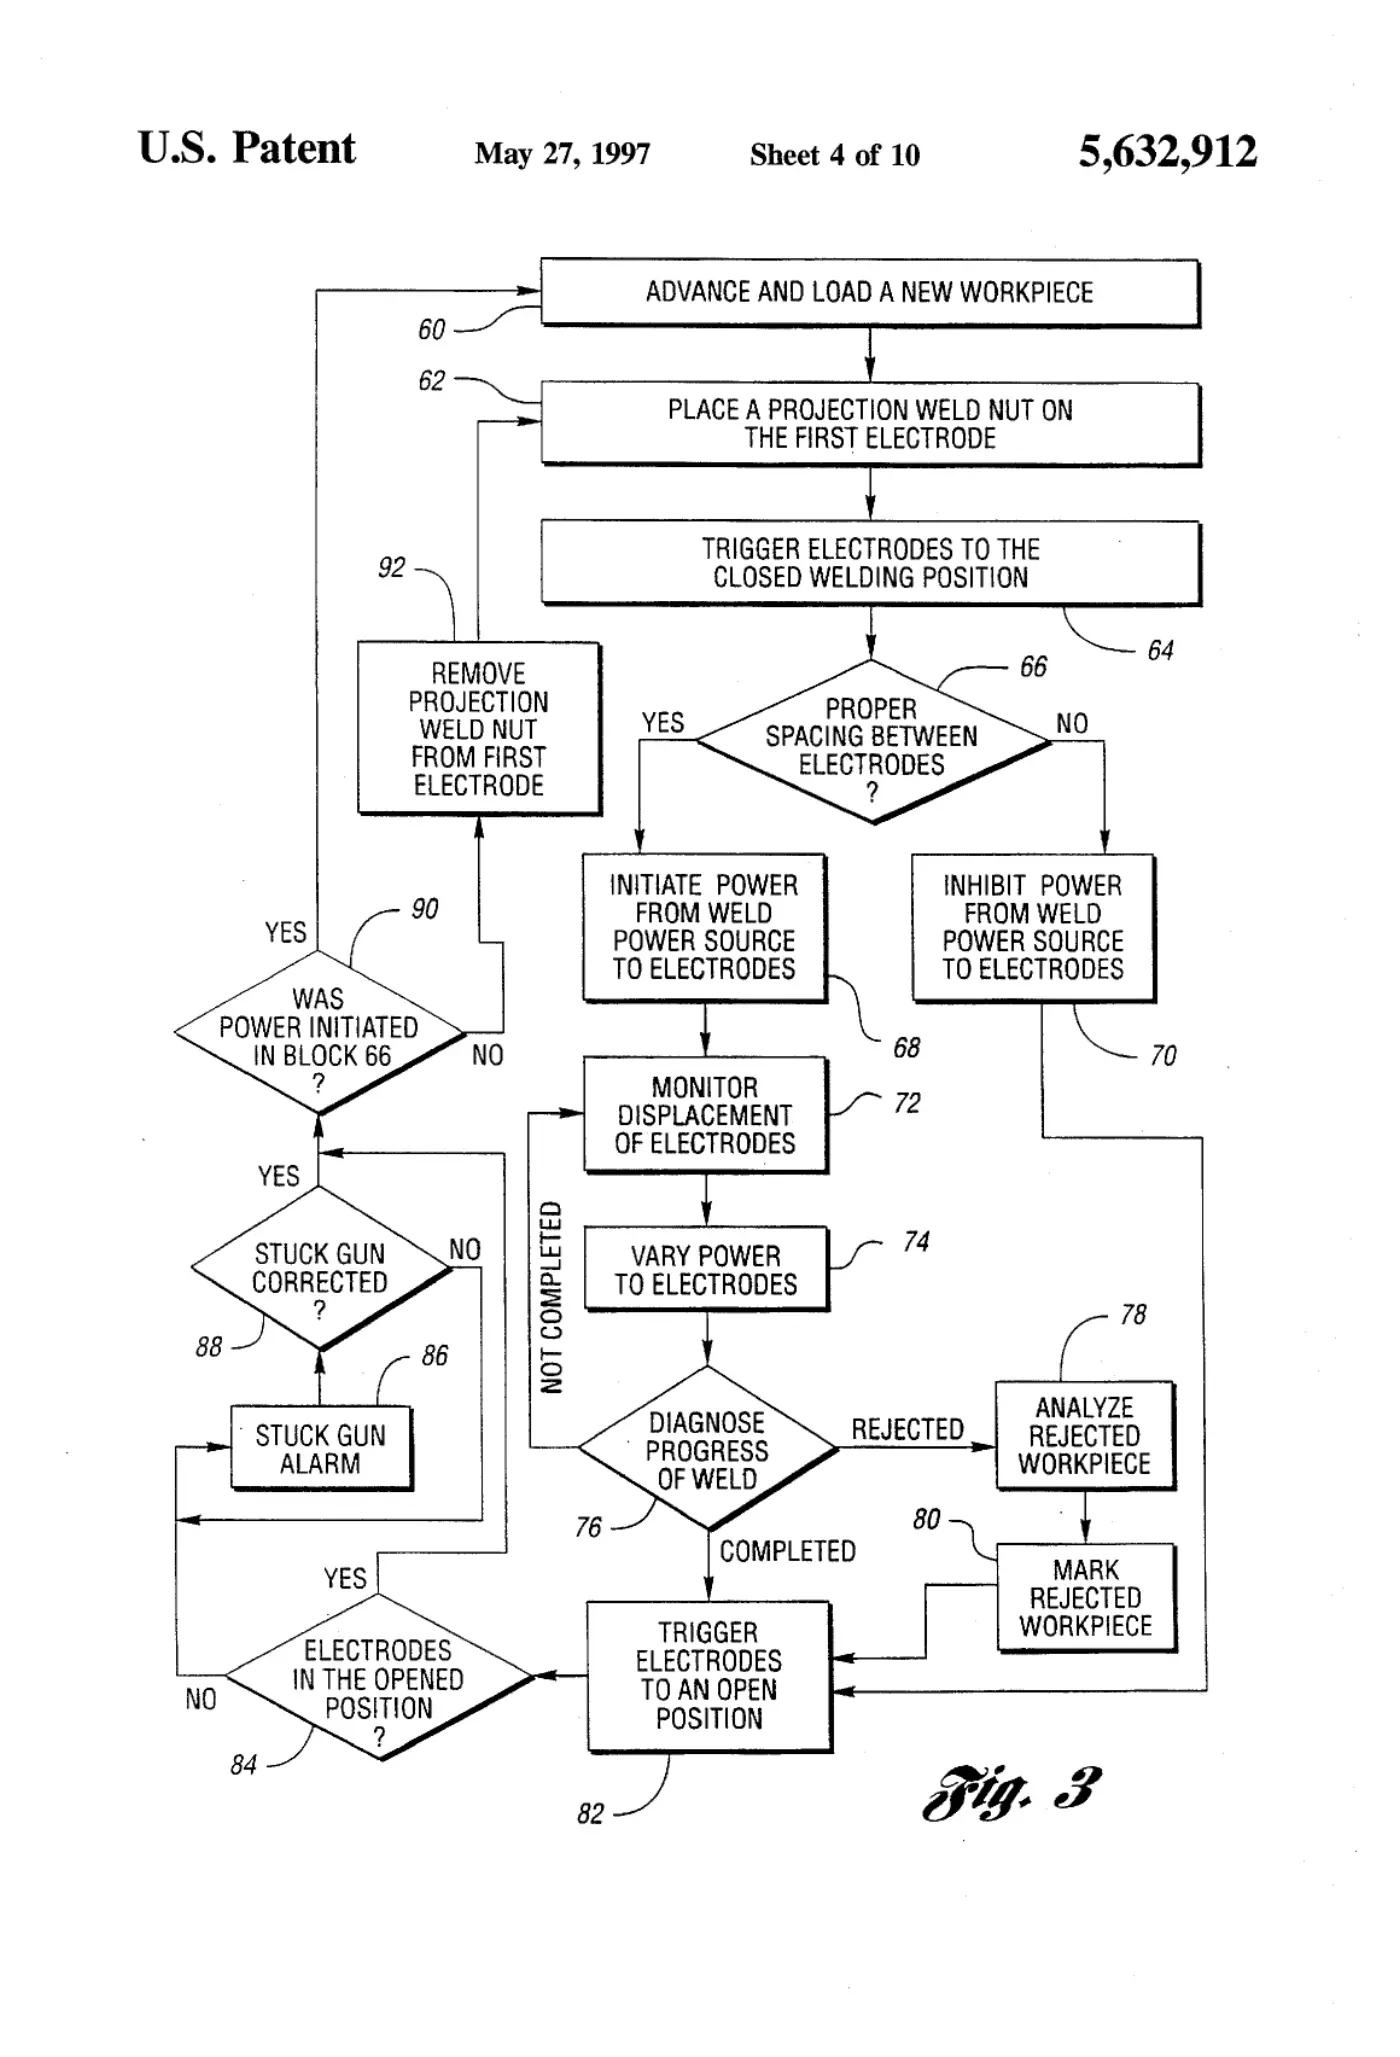
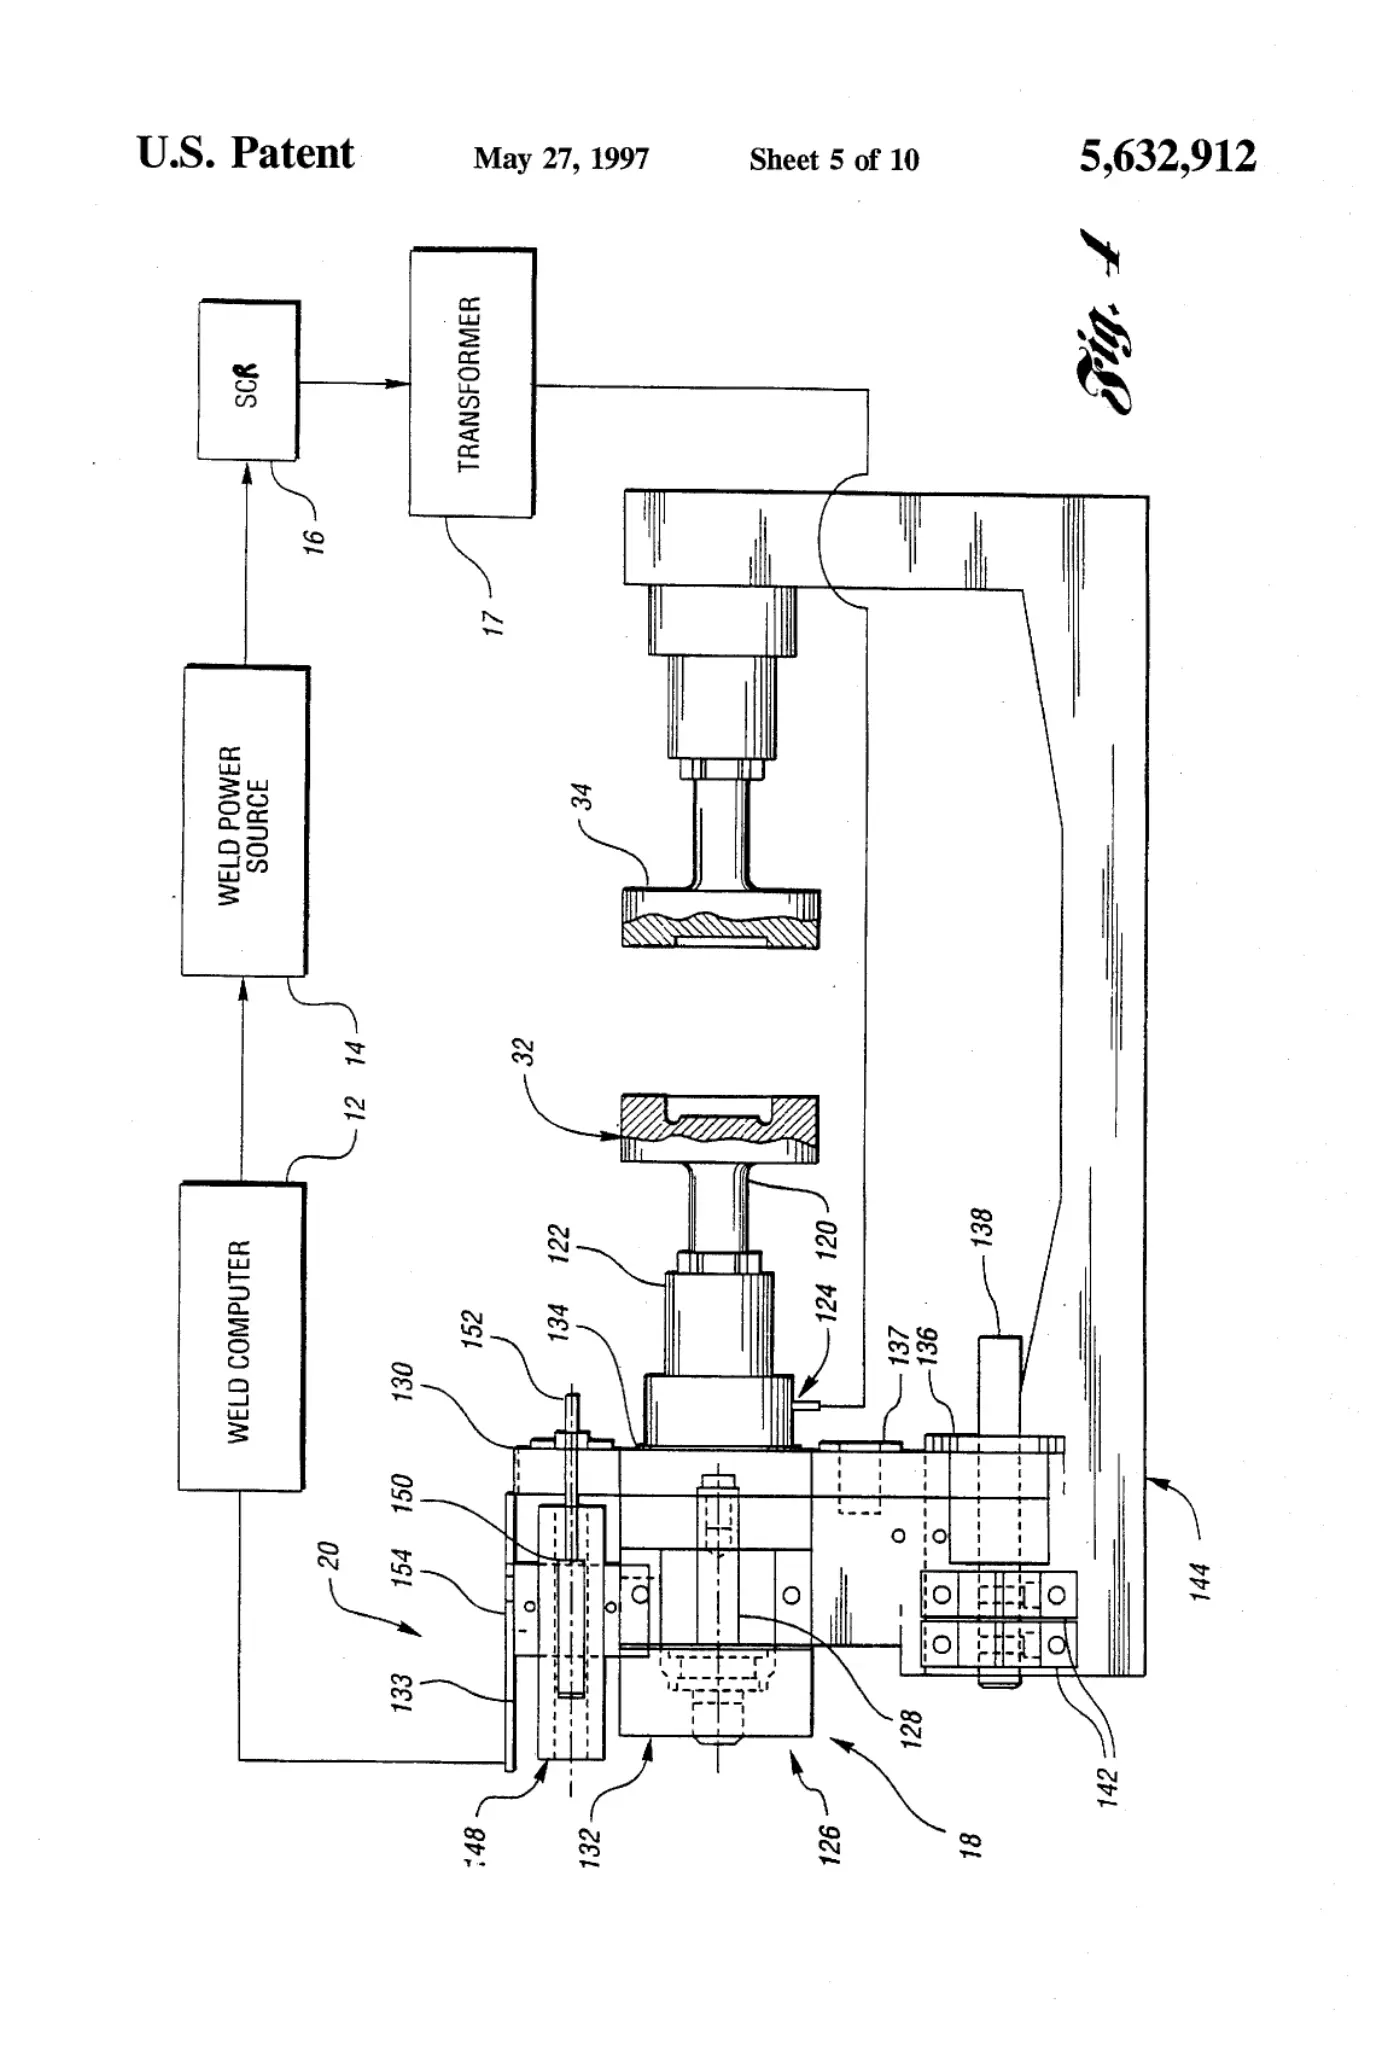
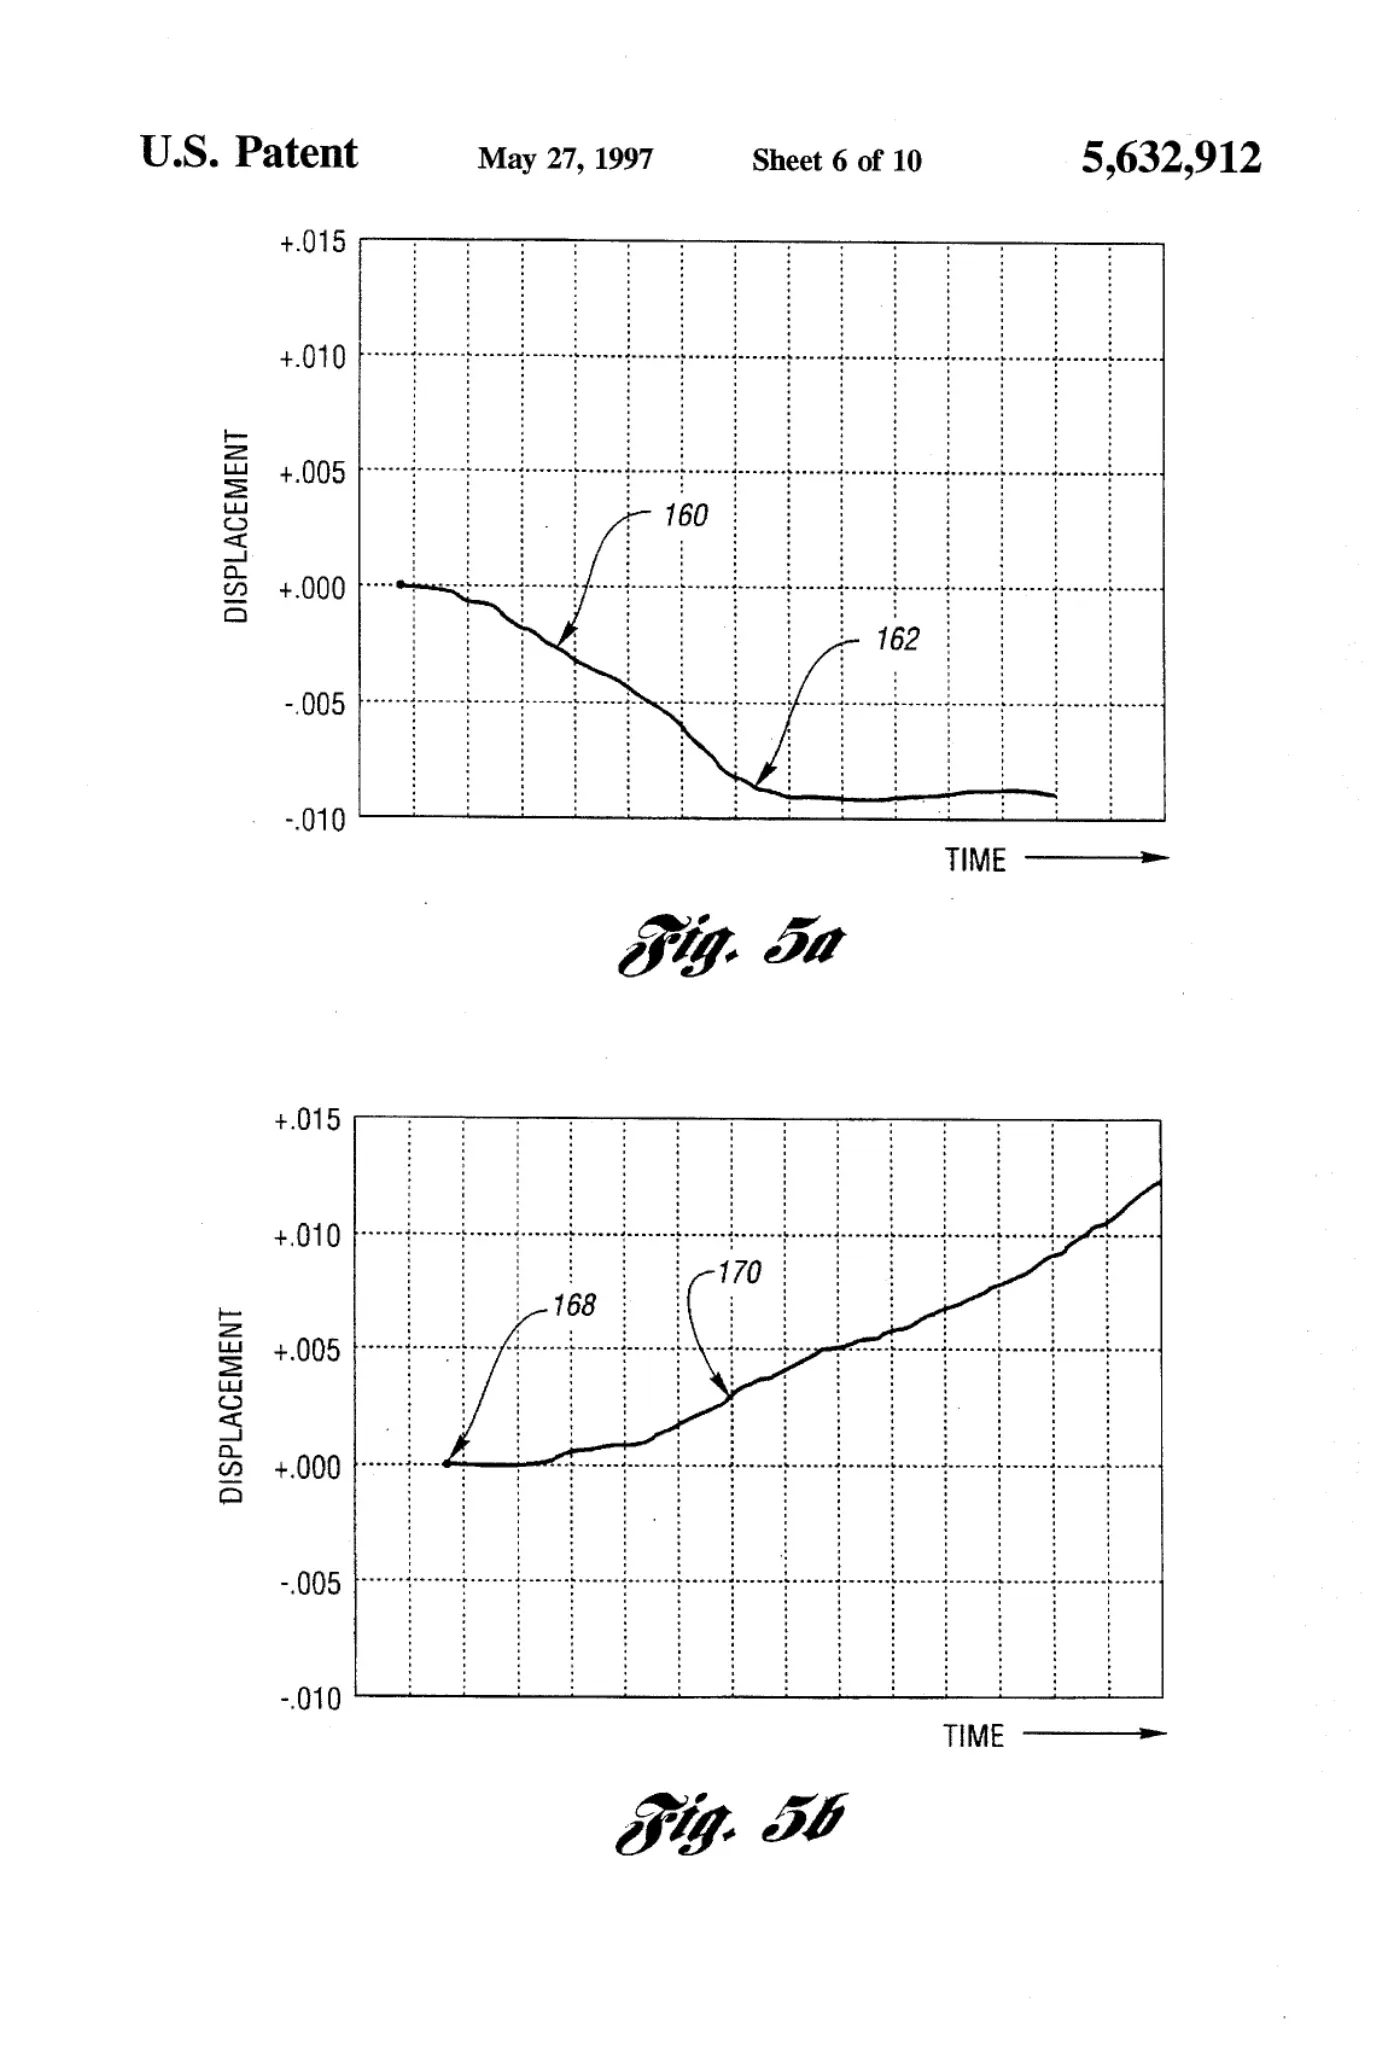
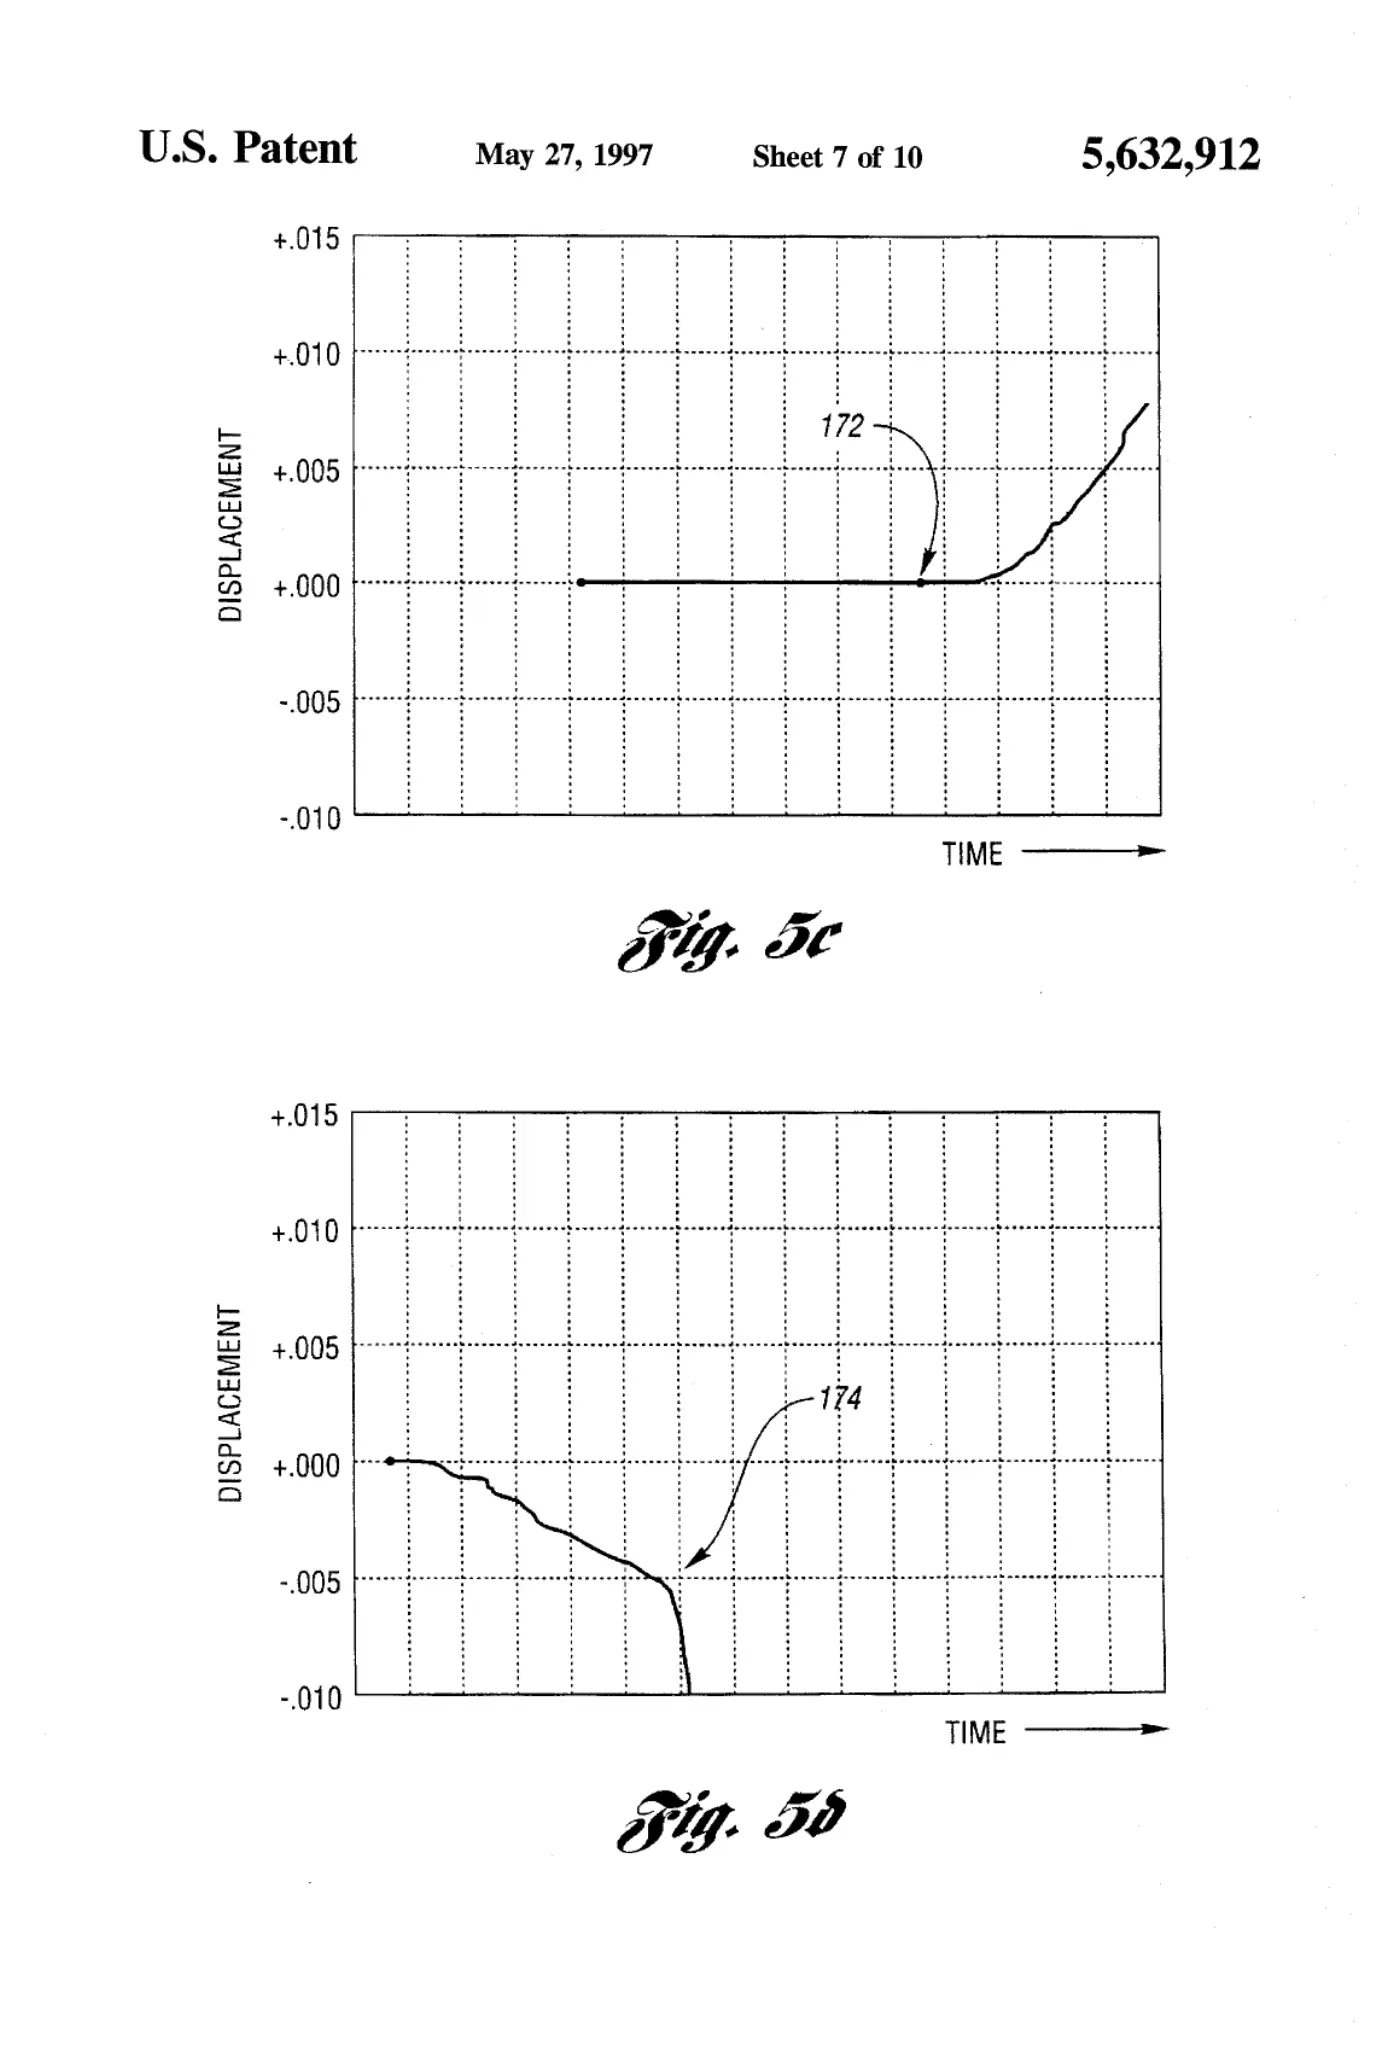
A system and method is disclosed for monitoring and controlling a resistance projection welder for welding a projection weld nut to a workpiece. A displacement sensor measures the displacement of a welding electrode of a weld gun in real time during the welding procedure. A computer is coupled to the displacement sensor and determines whether the projection weld nut is correctly loaded between the workpiece and the welding electrode. The computer instructs a programmable logic controller (PLC) to trigger a weld controller to apply power to the welding electrode if the projection weld nut is correctly loaded onto the workpiece. The computer instructs the PLC to inhibit power if it determines the projection weld nut to be inverted, missing, or misaligned in order to allow for the removal and replacement of the projection weld nut. The computer further instructs the PLC to control and terminate the power to the welding electrode in real time in order to form a projection weld between the projection weld nut and the workpiece that is substantially similar to a predetermined projection weld. The computer processes the displacement data and provides a fault signal when the projection weld is unacceptable. A marker marks the unacceptable workpieces in response to the fault signal.
Abstract
A system and method is disclosed for monitoring and controlling a resistance projection welder for welding a projection weld nut to a workpiece. A displacement sensor measures the displacement of a welding electrode of a weld gun in real time during the welding procedure. A computer is coupled to the displacement sensor and determines whether the projection weld nut is correctly loaded between the workpiece and the welding electrode. The computer instructs a programmable logic controller (PLC) to trigger a weld controller to apply power to the welding electrode if the projection weld nut is correctly loaded onto the workpiece. The computer instructs the PLC to inhibit power if it determines the projection weld nut to be inverted, missing, or misaligned in order to allow for the removal and replacement of the projection weld nut. The computer further instructs the PLC to control and terminate the power to the welding electrode in real time in order to form a projection weld between the projection weld nut and the workpiece that is substantially similar to a predetermined projection weld. The computer processes the displacement data and provides a fault signal when the projection weld is unacceptable. A marker marks the unacceptable workpieces in response to the fault signal.
1. Drawings
[0001]Sheet 1.
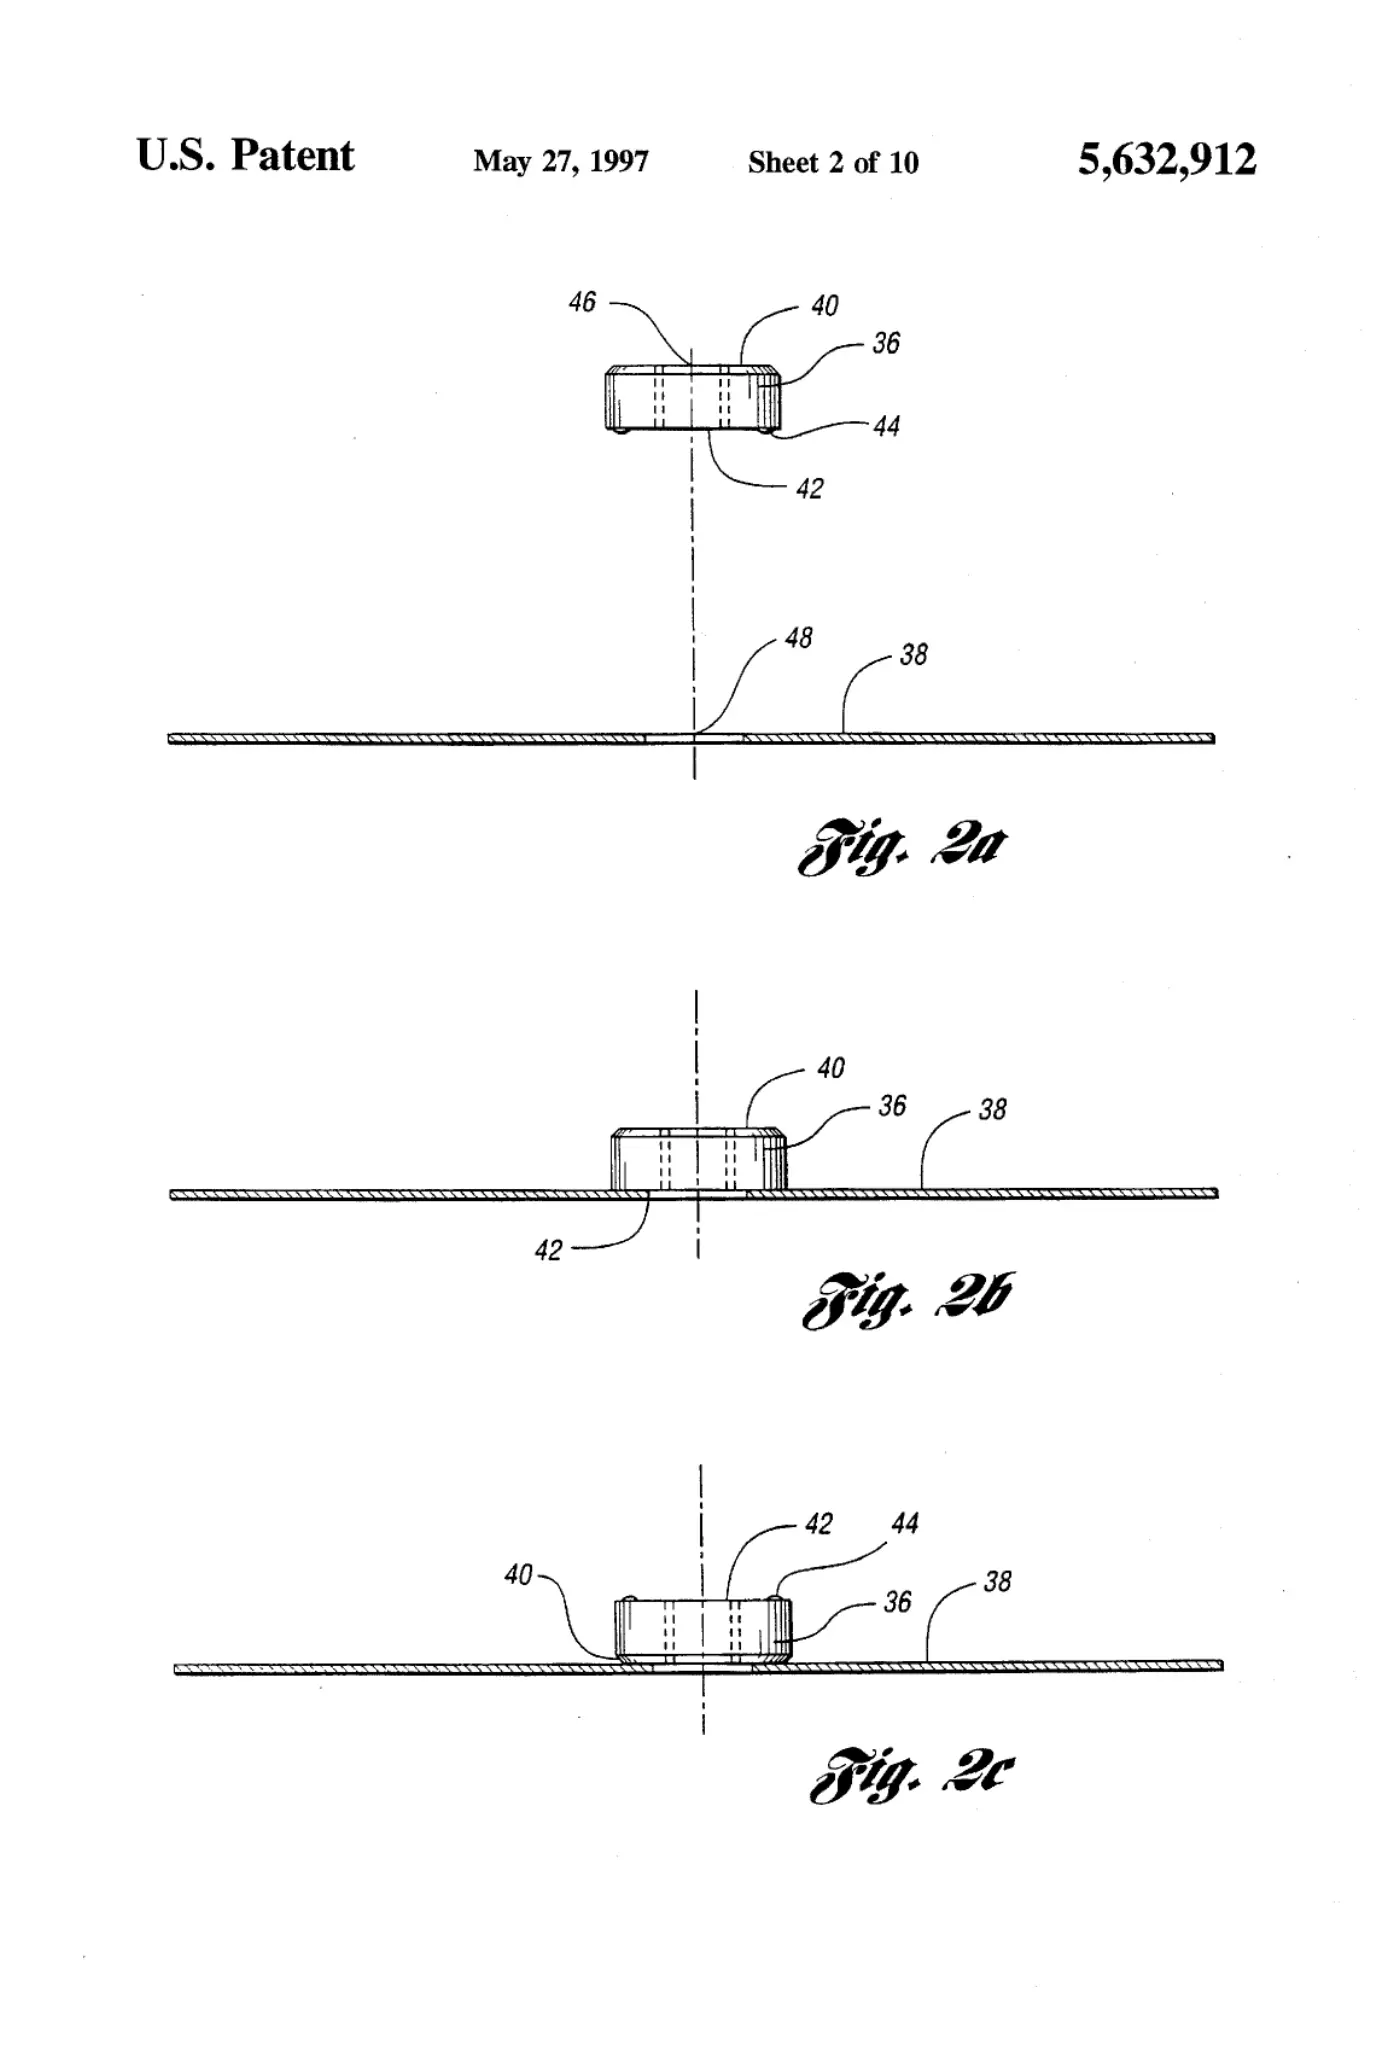
[0002]Sheet 2.
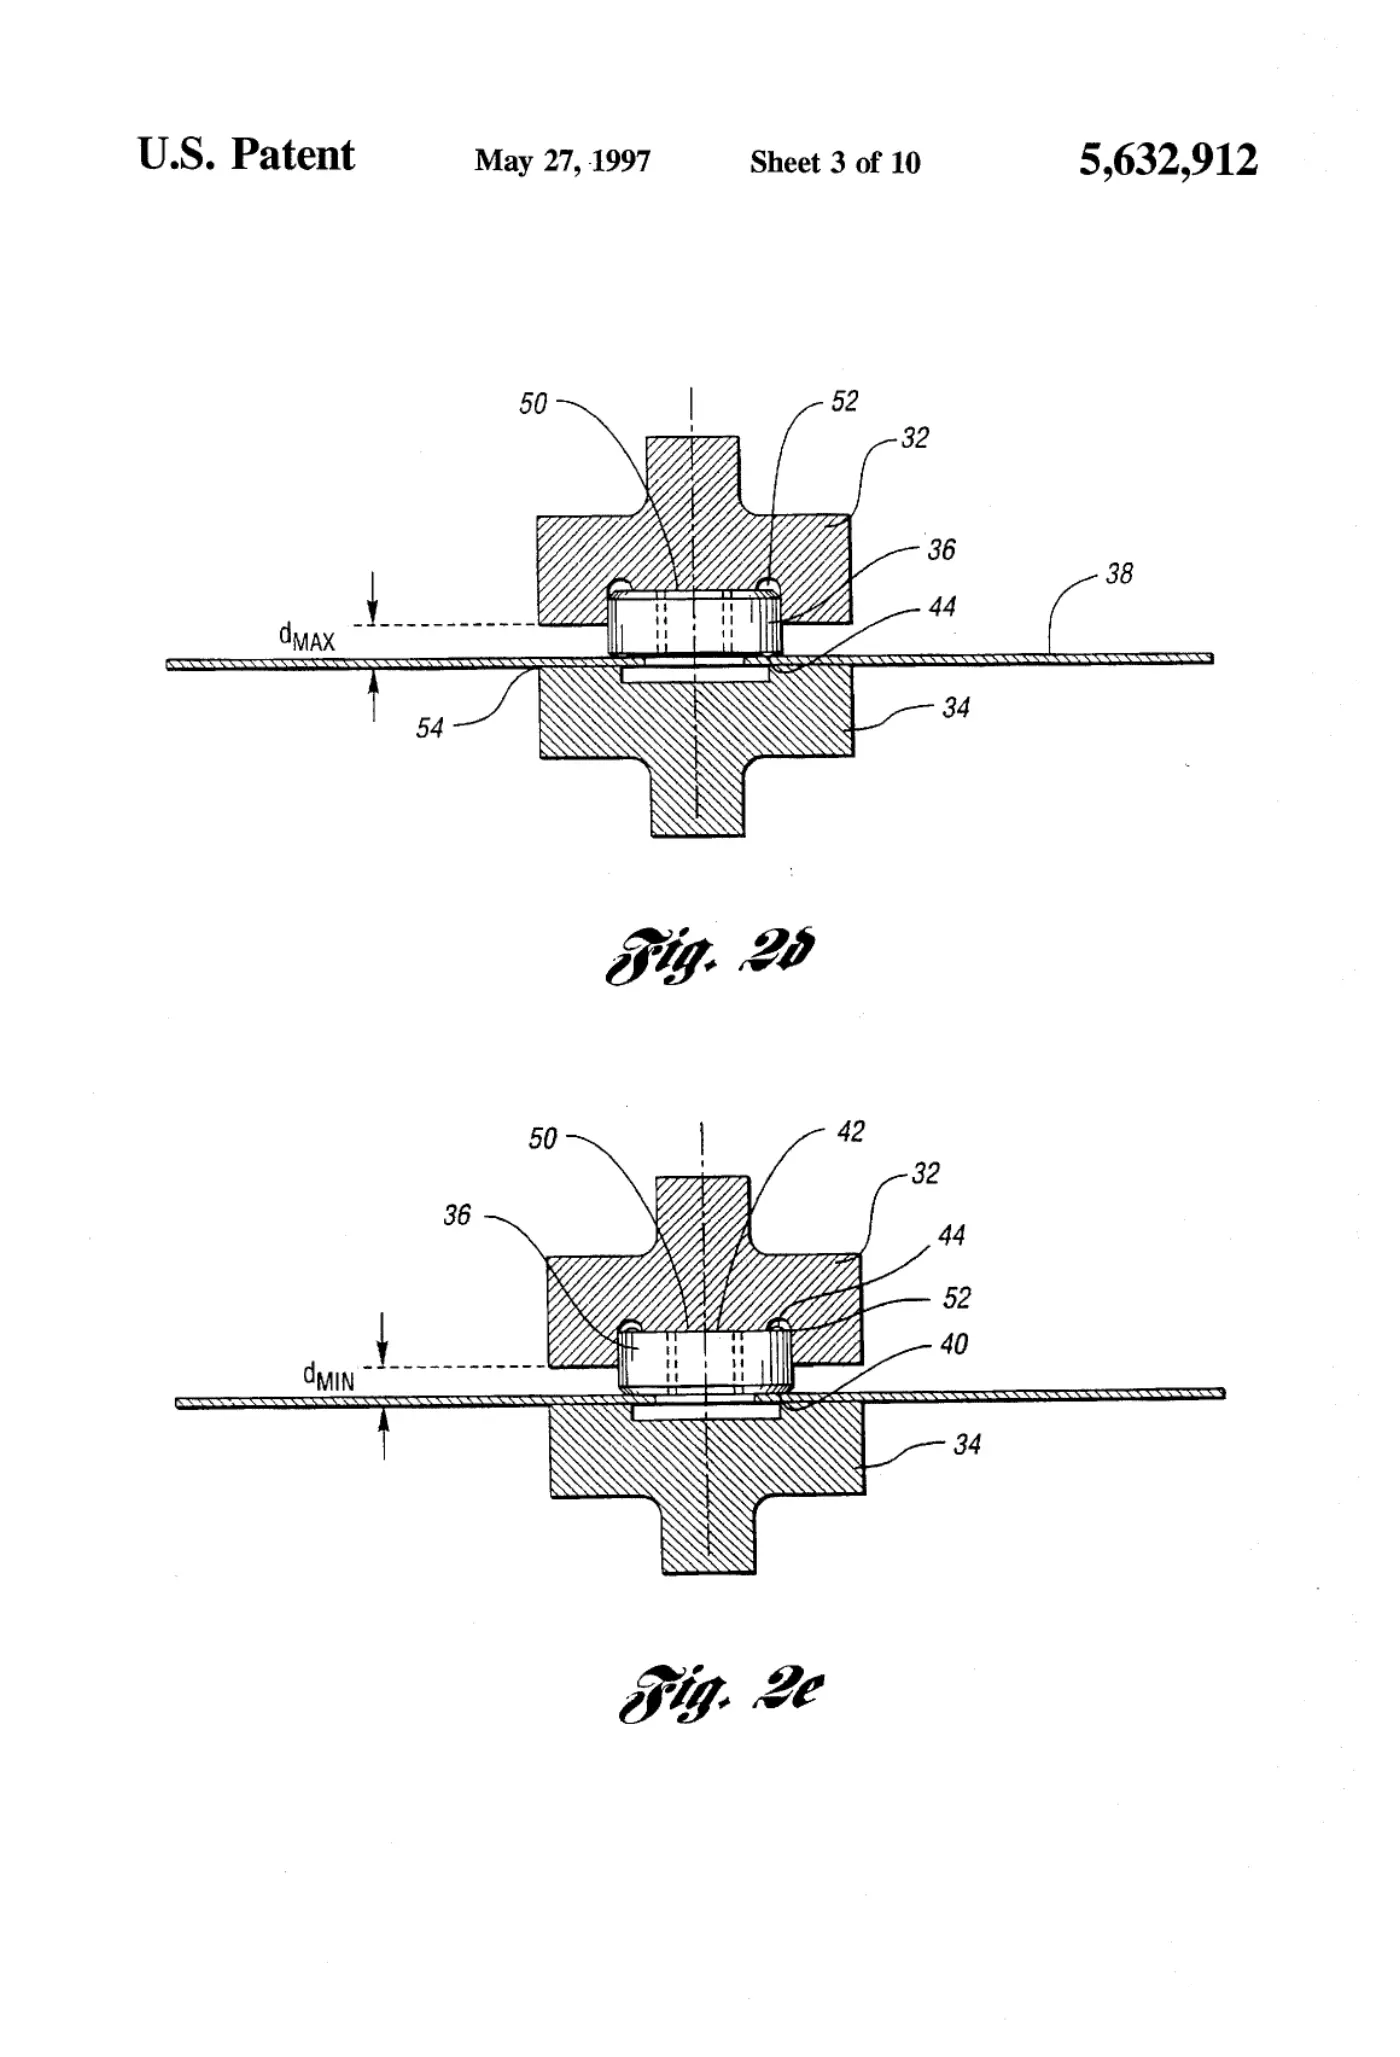
[0003]Sheet 3.
[0004]Sheet 4.
[0005]Sheet 5.
[0006]Sheet 6.
[0007]Sheet 7.
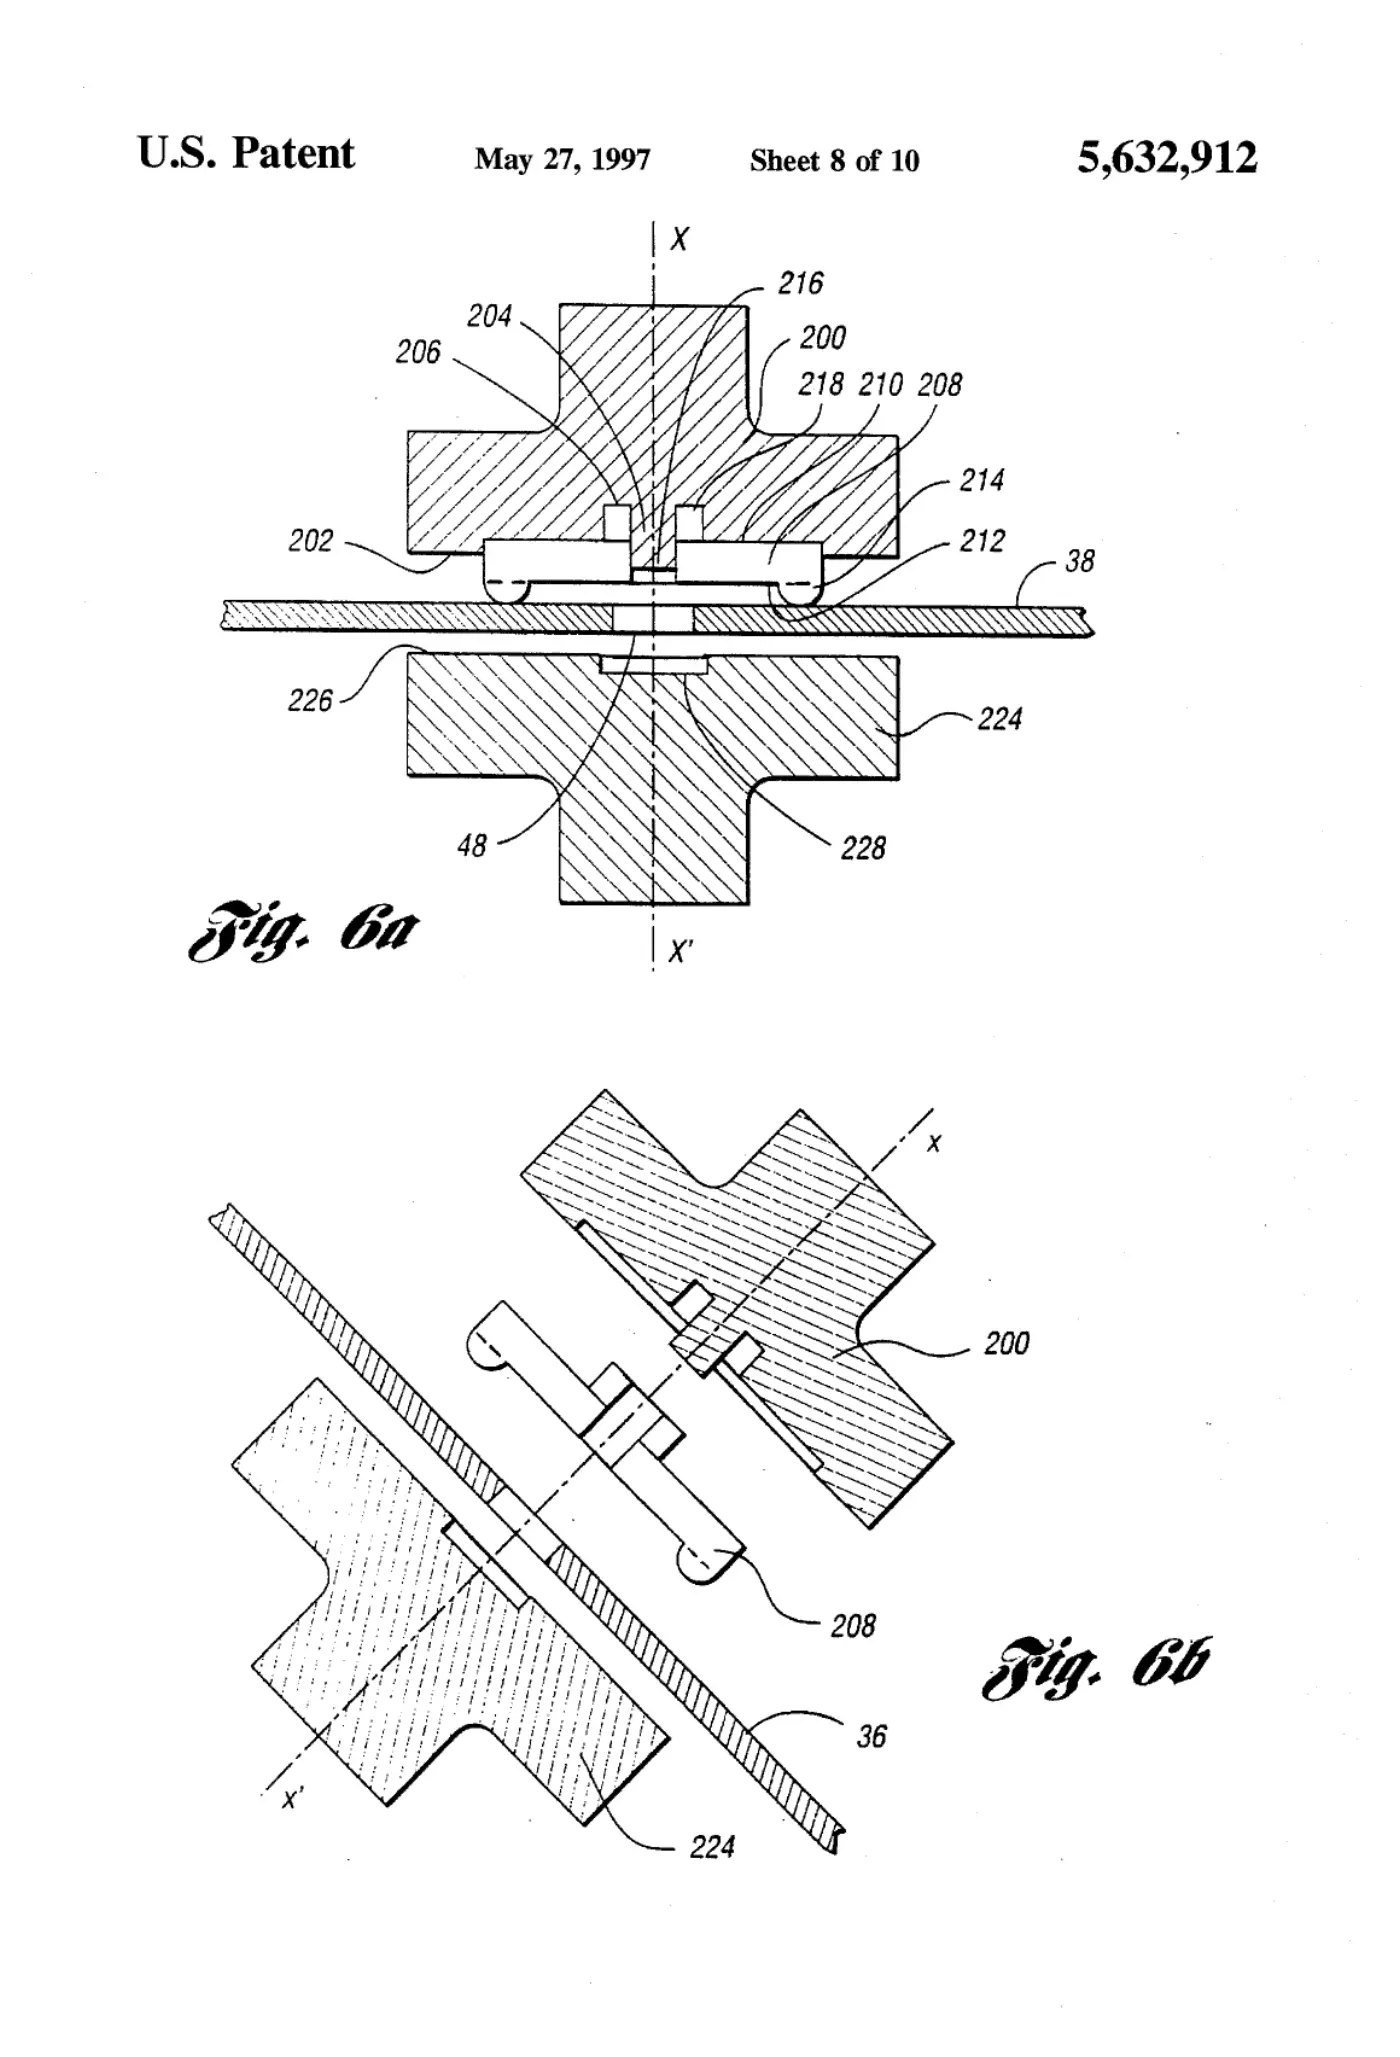
[0008]Sheet 8.
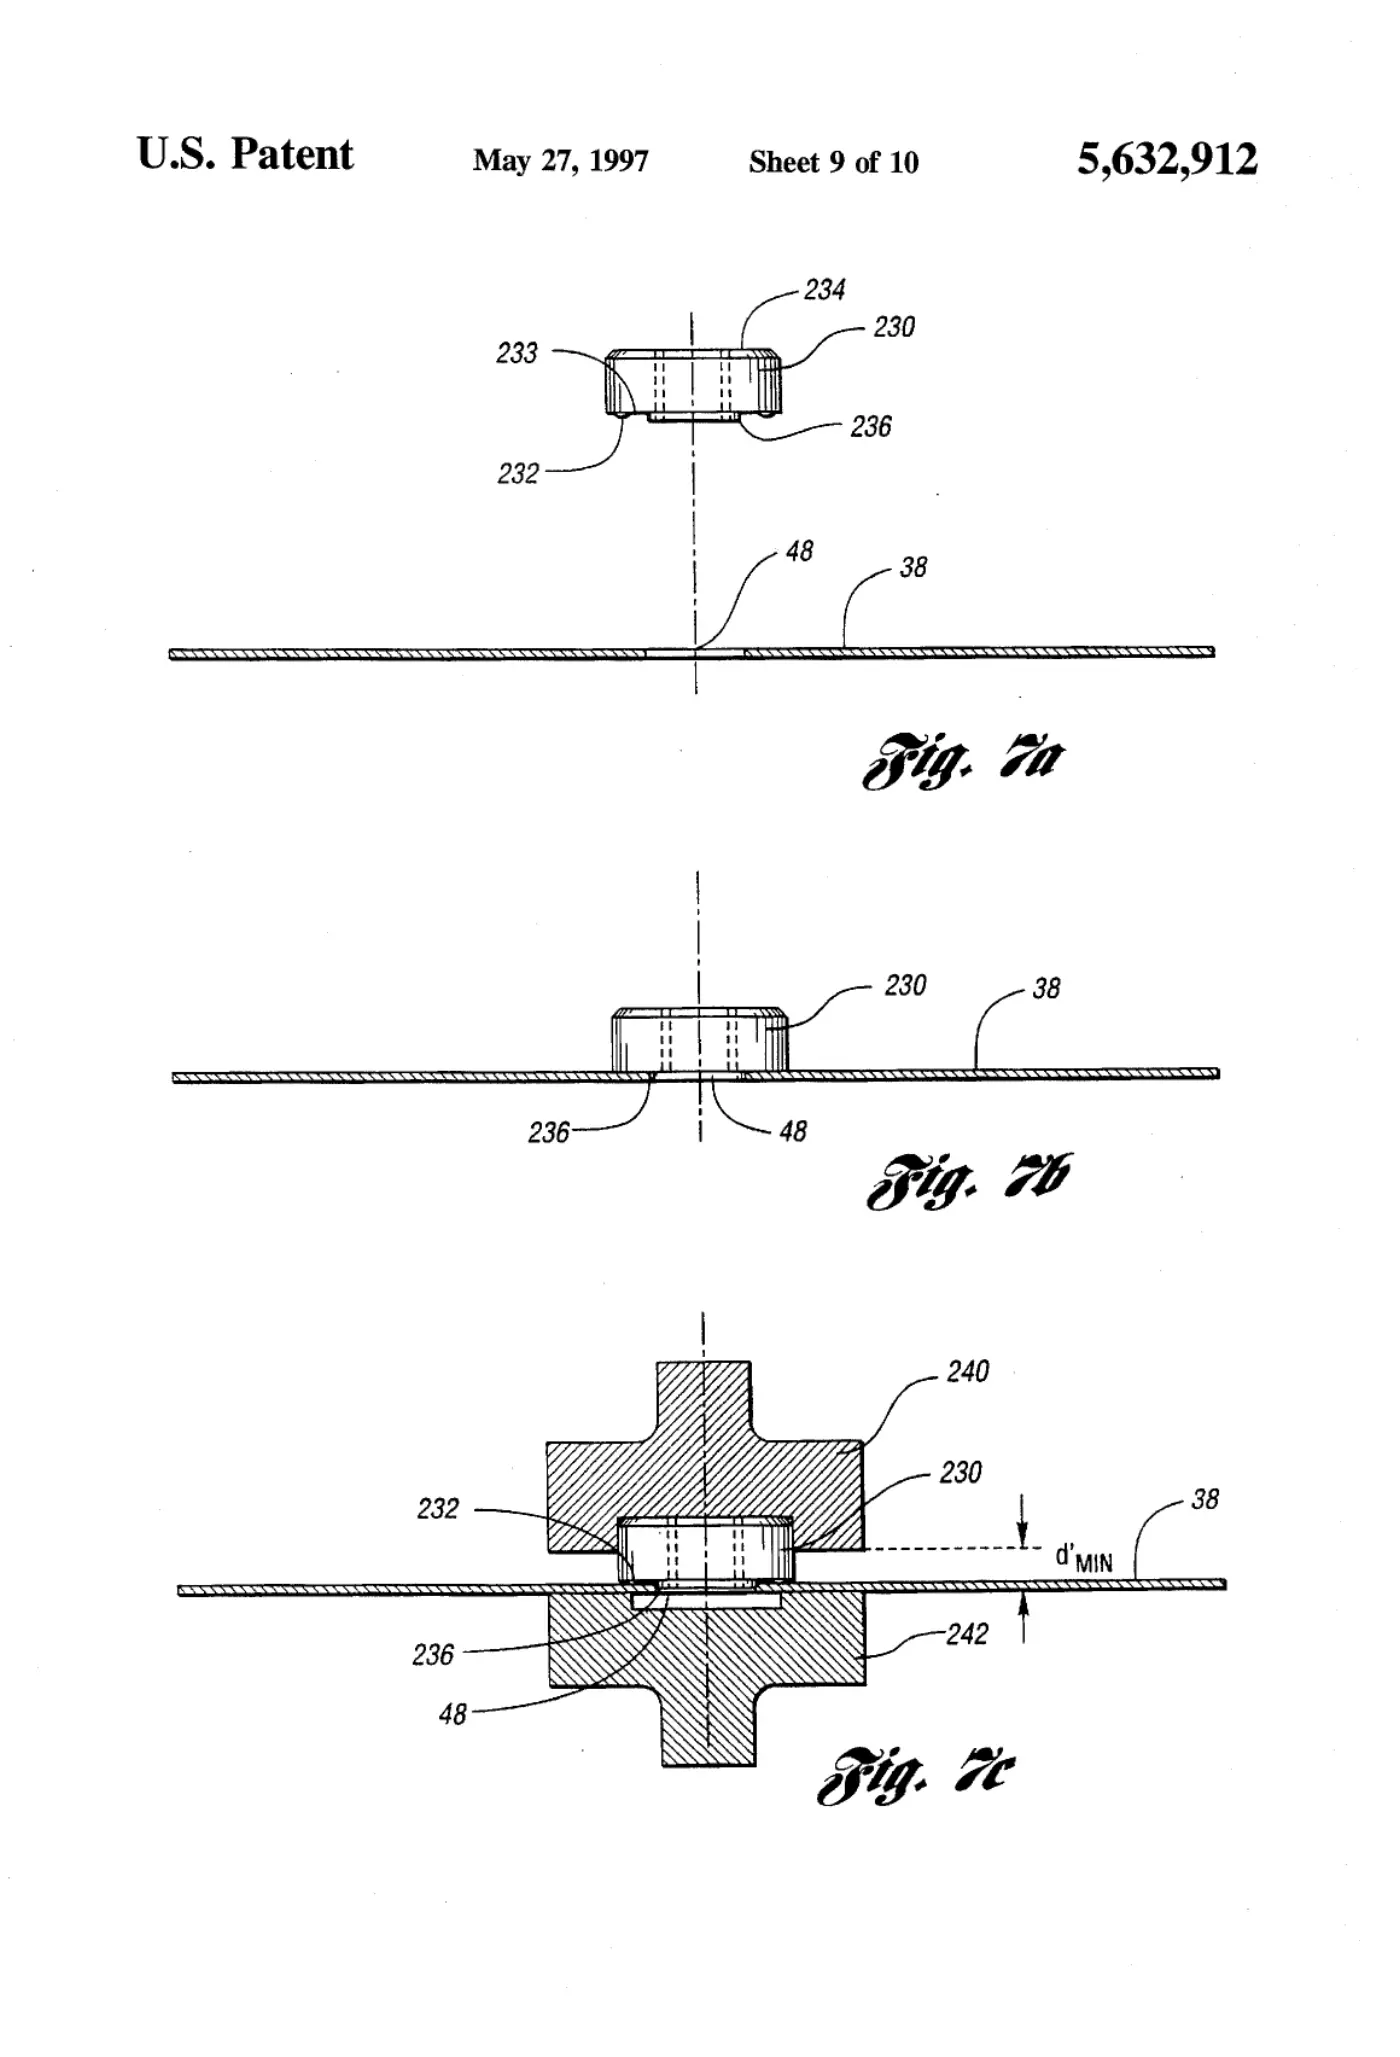
[0009]Sheet 9.
[0010]Sheet 10.
Publication information
Citation
OpenTechnical Publication OT-2026-000003258, “Resistance projection welding system and method for welding a projection weld nut to a workpiece,” published September 15, 2026 at 19:57:44 UTC, https://opentechnical.org/p/OT-2026-000003258.
To cite specific content, add the paragraph or figure numbers.
Terms
This record reproduces a document published elsewhere and is provided for reference and study. Rights in the original remain with its owner. See the publication policy.