OT-2026-000003326
Method for vacuum bag molding fiber reinforced resin matrix composites
- Published
- Permanent URL
- https://opentechnical.org/p/OT-2026-000003326
- Classification
- Lifting, Positioning & Manipulation › Vacuum Lifting
- Assignee
- MC DONNELL DOUGLAS CORP
- Original source
- US-5368807-A, the United States Patent and Trademark Office, 29 November 1994
- Document SHA-256
- b01fcfcb526ea06715e9314b9efeb852a8d917876c7b9b12dd0cddc33060df26
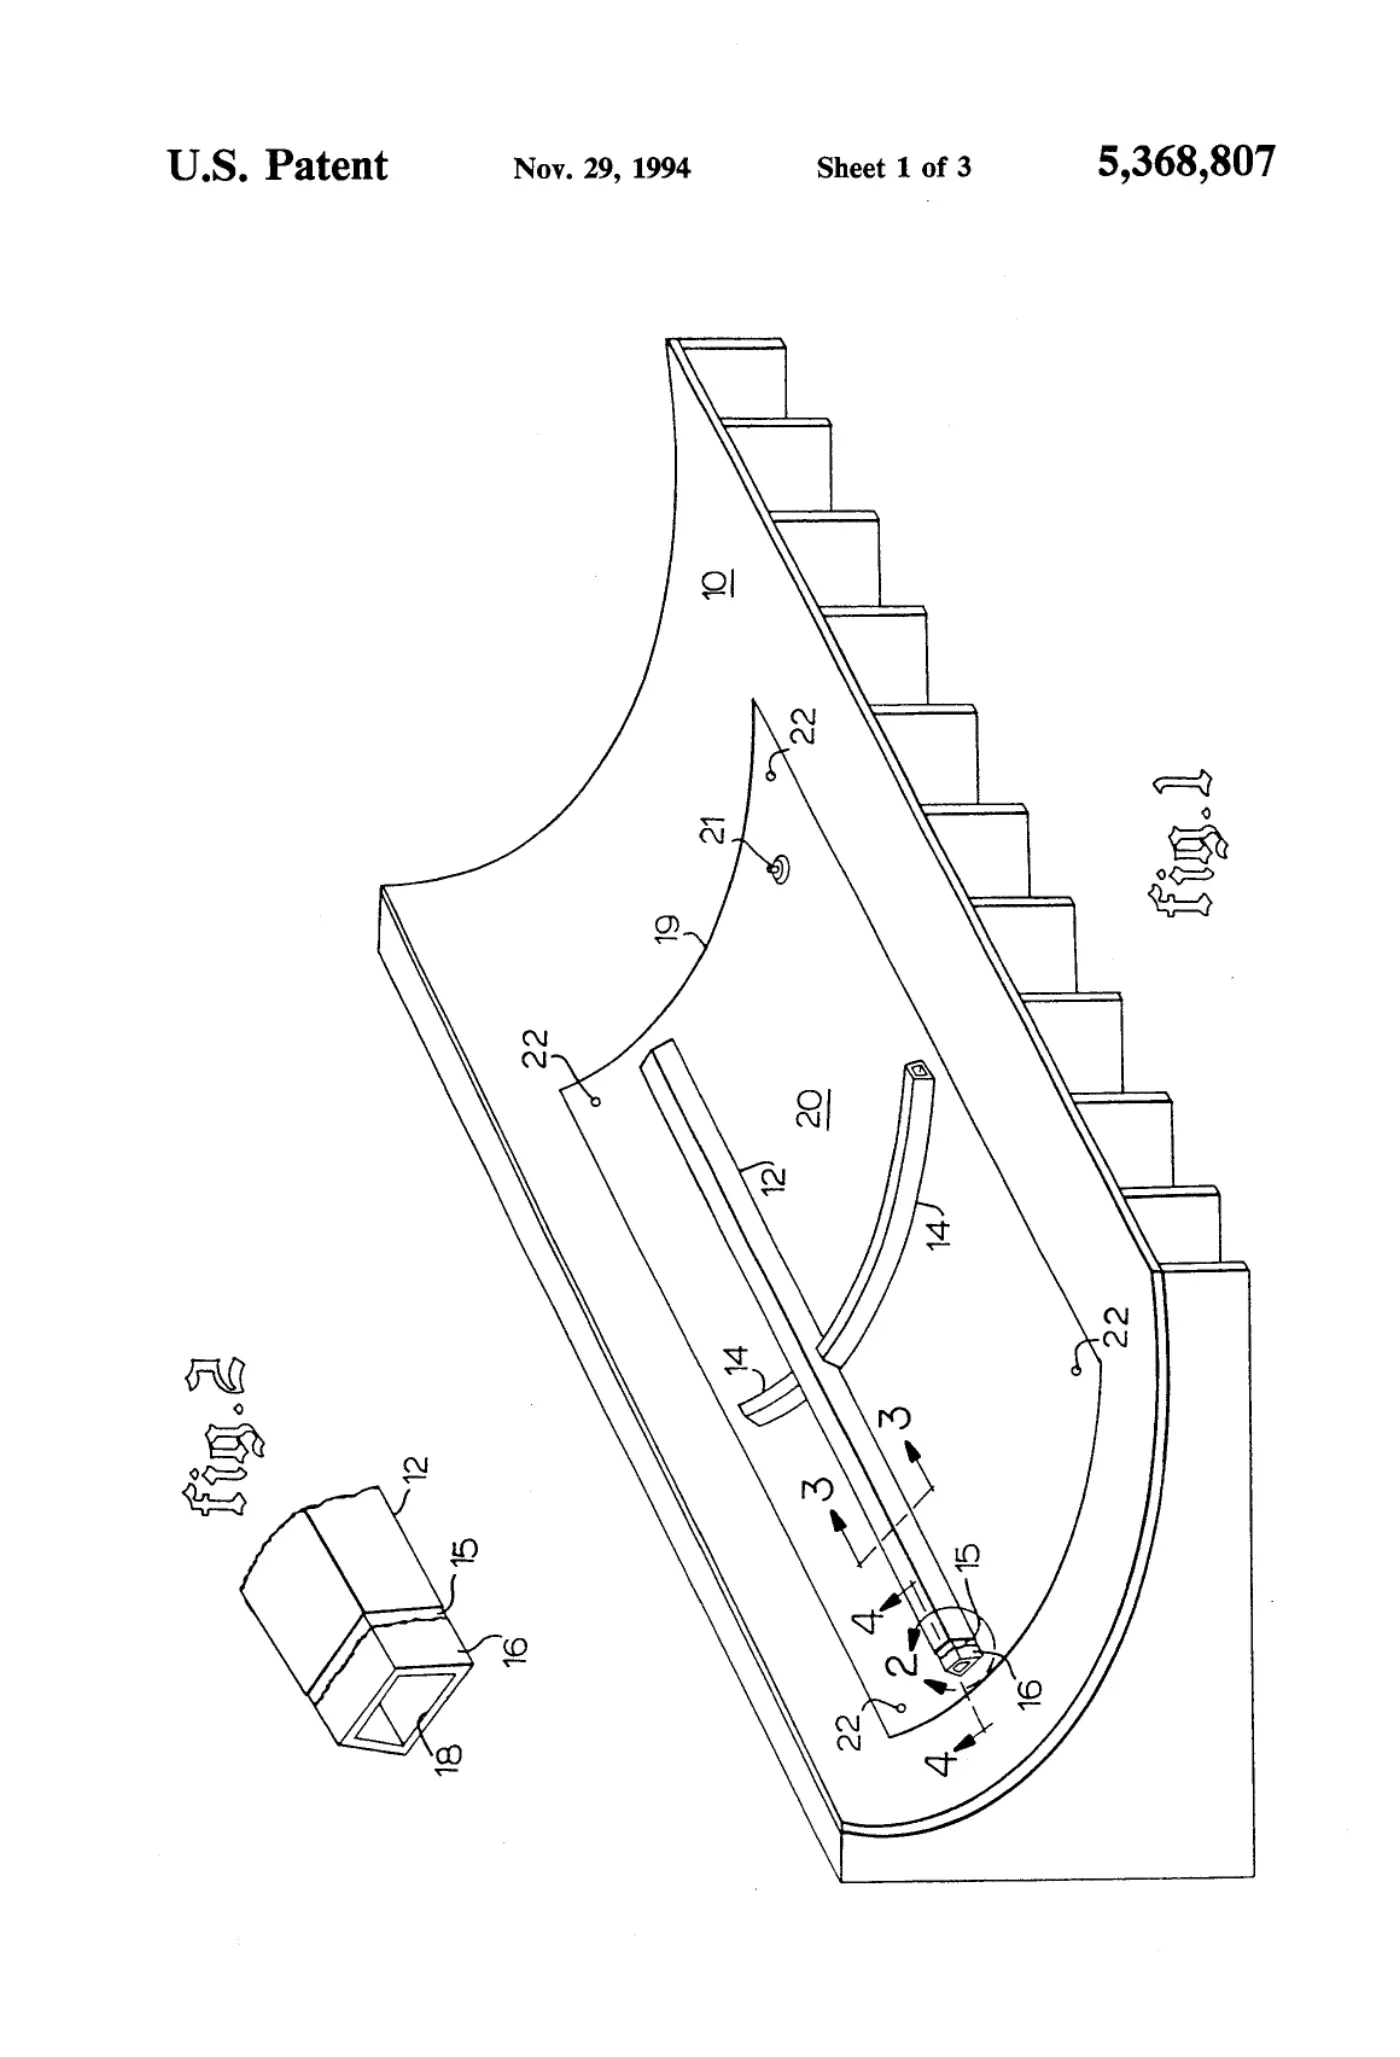
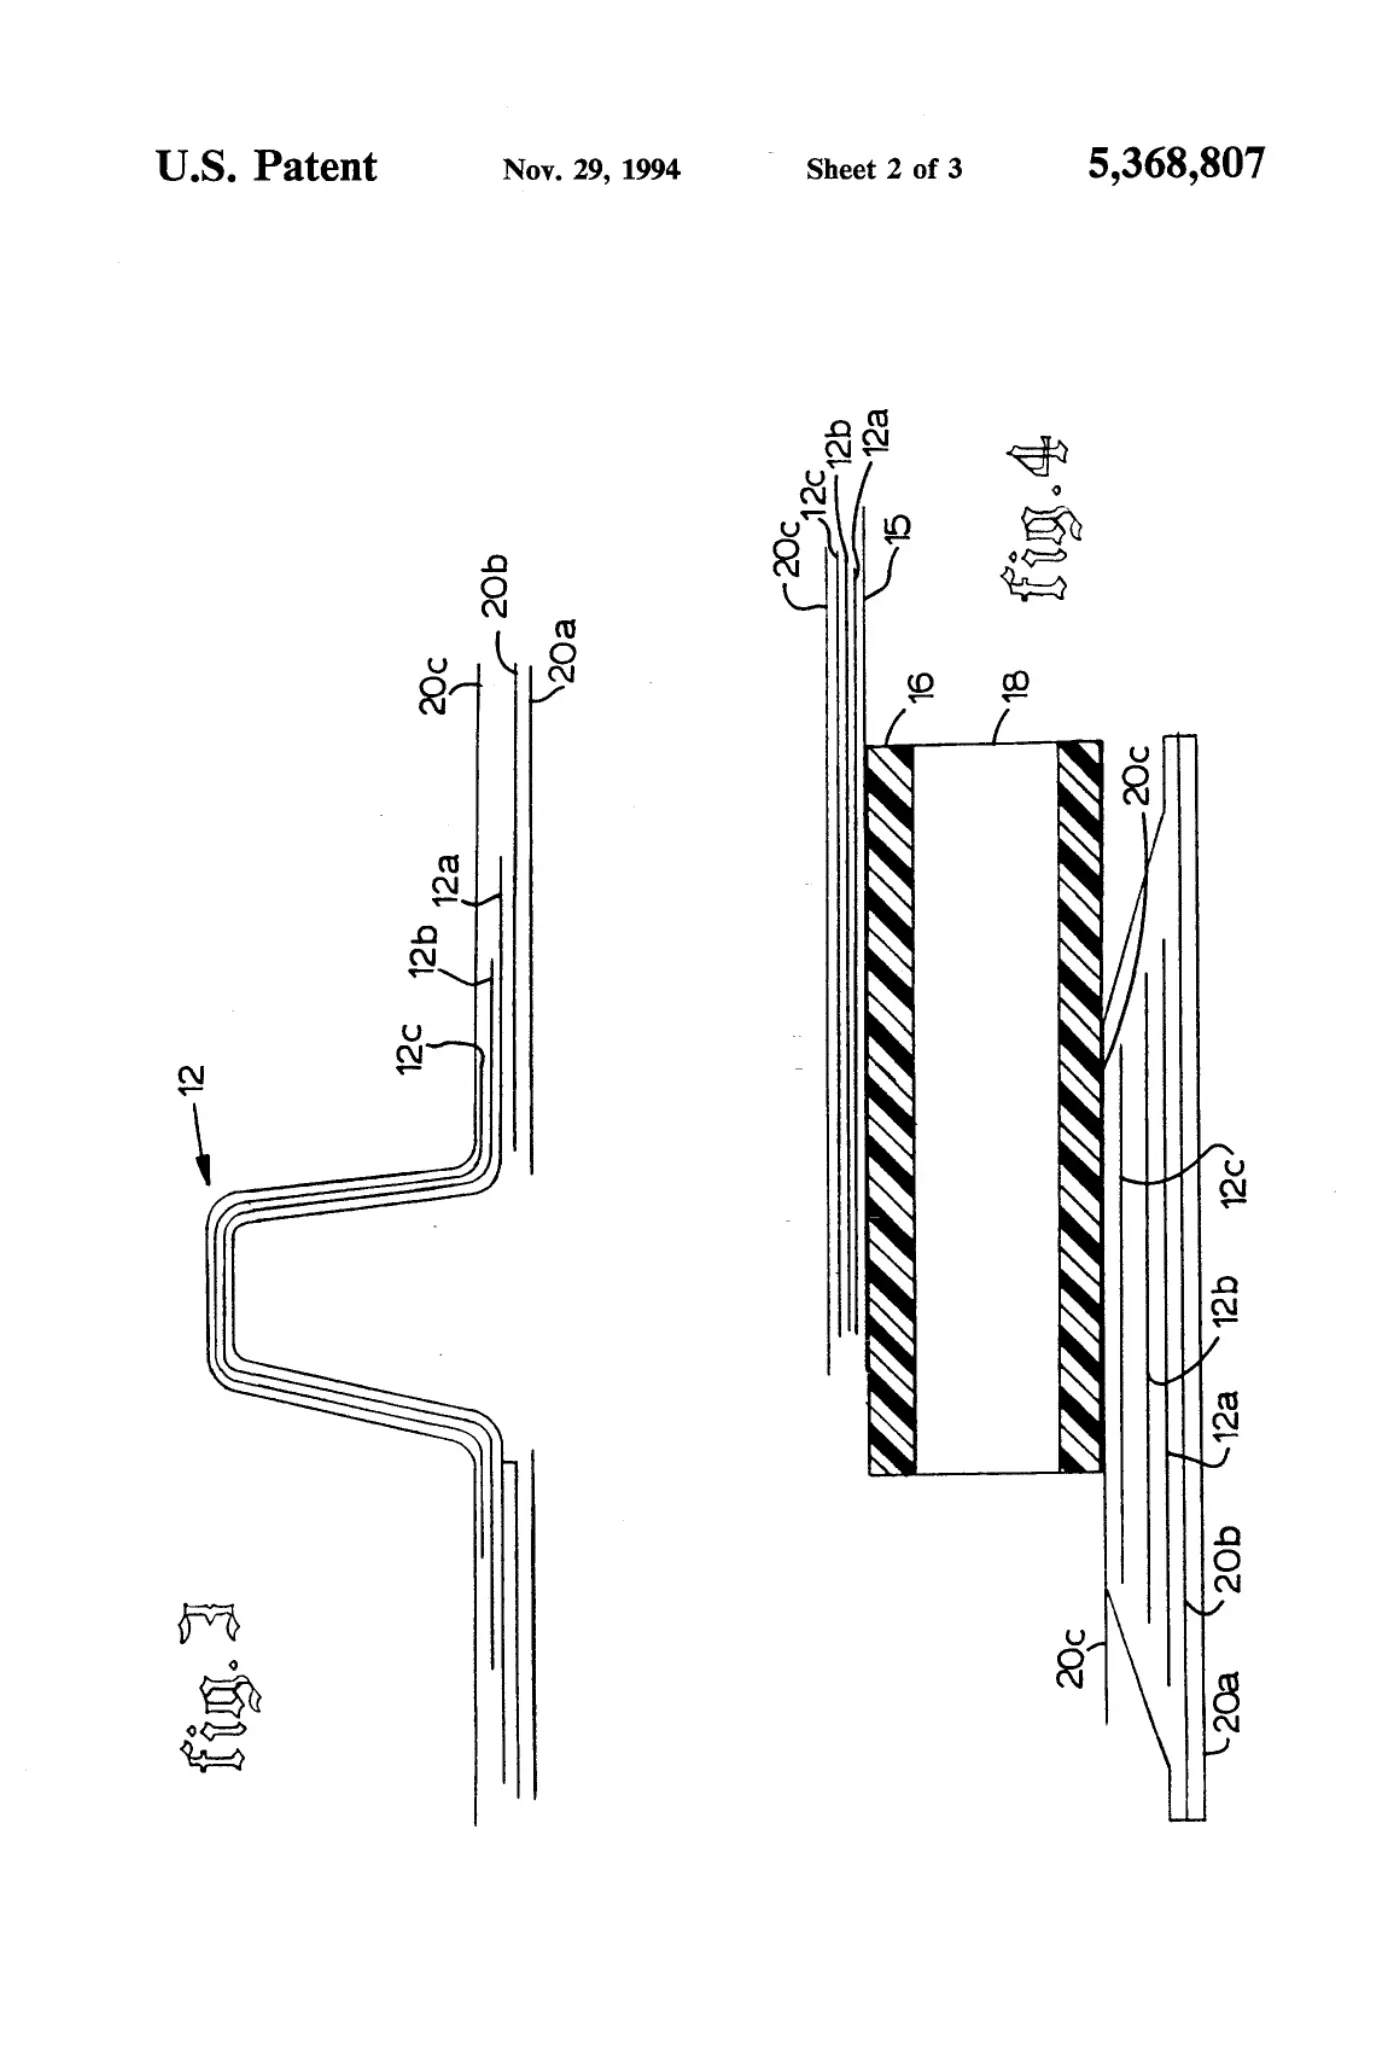
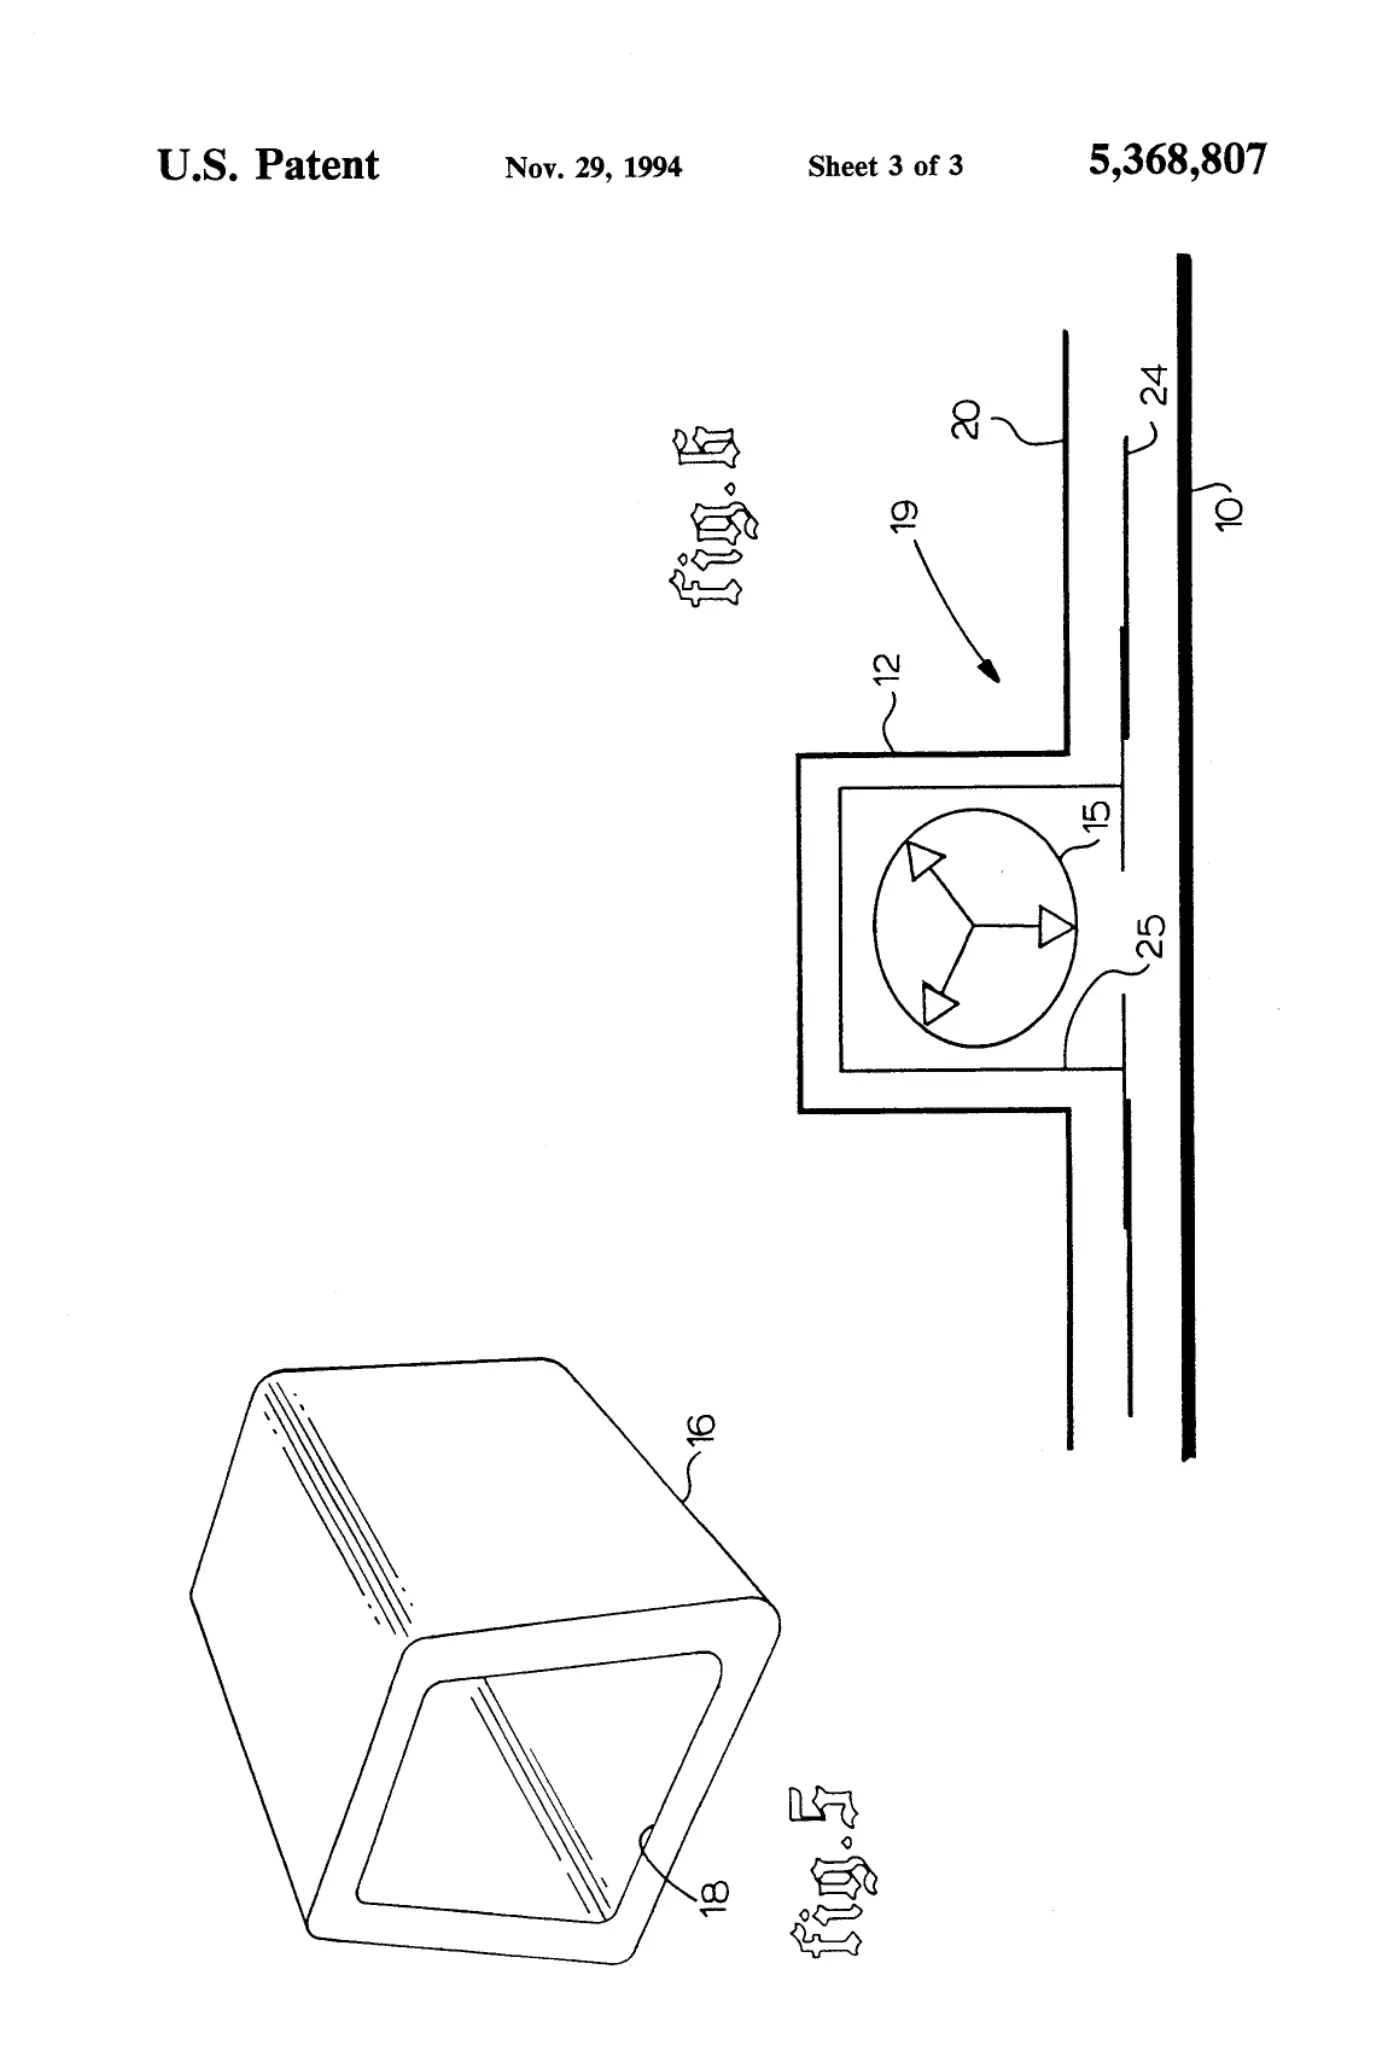
A method for fabricating fiber reinforced resin matrix composite structures having molded outside surfaces with intermittent molded inside surfaces (e.g. an aircraft skin with internal stiffeners) is performed as follows: composite prepreg stiffener sections are preformed and laid up on the inside portion of the rigid portion of the vacuum bag and the lay-up debulked. Elastomeric tubes are then installed in rigid cavity portions of a hybrid vacuum bag and sealing wedges are forced into place to hold the elastomeric tubes and at the same time seal them to the rigid portion of the cavity. The elastomeric tubes extend through and protrude from the sealing wedges. Skin plies are then laid up on a primary mold and the hybrid bag installed on the mold. Index pins are provided to properly orient the hybrid bag to the primary mold or tool. A vacuum is then drawn on the bag, any vacuum leaks are remedied, and the part is ready for curing in either an oven or an autoclave. After curing, the sealing wedges are removed and a vacuum is drawn on the elastomeric tubes to collapse them for easy removal. After removal of the elastomeric tubes and the hybrid bag the completed structural part is removed from the primary tool.
Abstract
A method for fabricating fiber reinforced resin matrix composite structures having molded outside surfaces with intermittent molded inside surfaces (e.g. an aircraft skin with internal stiffeners) is performed as follows: composite prepreg stiffener sections are preformed and laid up on the inside portion of the rigid portion of the vacuum bag and the lay-up debulked. Elastomeric tubes are then installed in rigid cavity portions of a hybrid vacuum bag and sealing wedges are forced into place to hold the elastomeric tubes and at the same time seal them to the rigid portion of the cavity. The elastomeric tubes extend through and protrude from the sealing wedges. Skin plies are then laid up on a primary mold and the hybrid bag installed on the mold. Index pins are provided to properly orient the hybrid bag to the primary mold or tool. A vacuum is then drawn on the bag, any vacuum leaks are remedied, and the part is ready for curing in either an oven or an autoclave. After curing, the sealing wedges are removed and a vacuum is drawn on the elastomeric tubes to collapse them for easy removal. After removal of the elastomeric tubes and the hybrid bag the completed structural part is removed from the primary tool.
1. Drawings
[0001]Sheet 1.
[0002]Sheet 2.
[0003]Sheet 3.
Publication information
Citation
OpenTechnical Publication OT-2026-000003326, “Method for vacuum bag molding fiber reinforced resin matrix composites,” published September 15, 2026 at 20:09:47 UTC, https://opentechnical.org/p/OT-2026-000003326.
To cite specific content, add the paragraph or figure numbers.
Terms
This record reproduces a document published elsewhere and is provided for reference and study. Rights in the original remain with its owner. See the publication policy.